창립자에게 문의하기
아직도 궁금한 점이 있으신가요?
저희 창립자와 직접 연결하세요. 가격이든 기술적인 세부 사항이든 명확한 답변을 받고, 첫 주문을 위한 독점 ‘창립자 보너스’도 받아보세요.
900명 이상의 만족 고객
🏆 1,000건 이상의 맞춤 프로젝트를 성공적으로 납품했습니다.
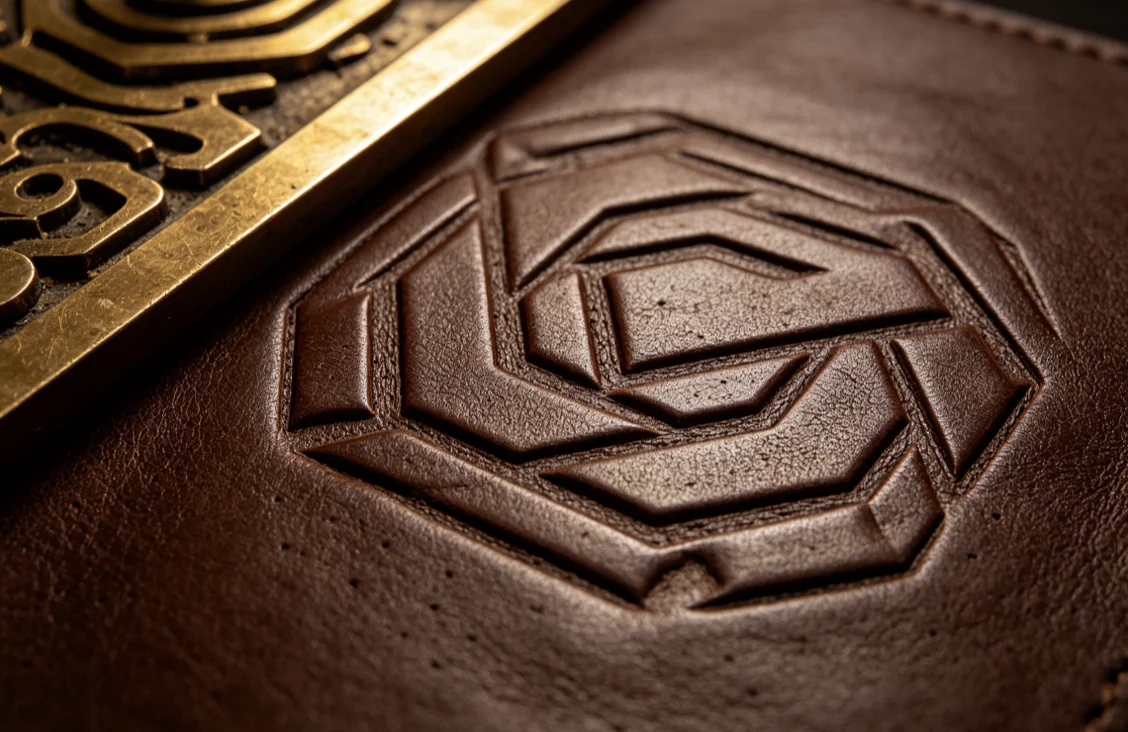
A practical temperature test for large-area leather 3D embossing on the YTJ-5T hydraulic hot stamping press, with the cleanest result at 110°C.
If you are trying to emboss a large leather panel, the first thing you need to get right is not the logo or the mold pattern. It is the heat balance.
In our YTJ-5T hydraulic hot stamping press test, the cleanest large-area leather 3D embossing result came at 110°C with about 2 seconds of dwell time. At 90°C, the relief was too soft. At 130°C and 150°C, the surface started to show gloss, shrinkage, edge spread, and loss of fine detail.
This article is for leather goods manufacturers, sample developers, and production managers who need a practical setting for 3D relief work on wallets, bags, notebook covers, belts, and other large leather surfaces.
Leather is a natural material, embossing is a pressure-and-heat forming process, and hot stamping combines both heat and pressure to create a permanent surface effect. That means a small temperature change can make a big visual difference. For background reading, see 가죽, Embossing, 및 Hot stamping.
For large-area leather 3D embossing, the best starting point is 110°C / 2 seconds on the YTJ-5T hydraulic hot stamping press. It gives the strongest balance between depth, edge definition, and surface stability.
If you go lower, the relief may not fully form. If you go higher, the leather surface can become shiny or slightly deformed, especially on broad areas where the heat has more time to spread.
Small logos and large relief patterns do not behave the same way.
With a small stamp, heat and pressure stay concentrated in one tight area. With a large embossing pattern, the leather must hold the form across a wider surface, so the grain, moisture, coating, and thickness all matter more. If the temperature is too low, the center may form but the edges stay weak. If the temperature is too high, the outer area can overreact before the full pattern is fully set.
That is why large-area leather embossing is less forgiving than simple one-line branding. You are not just making a mark. You are shaping a surface.
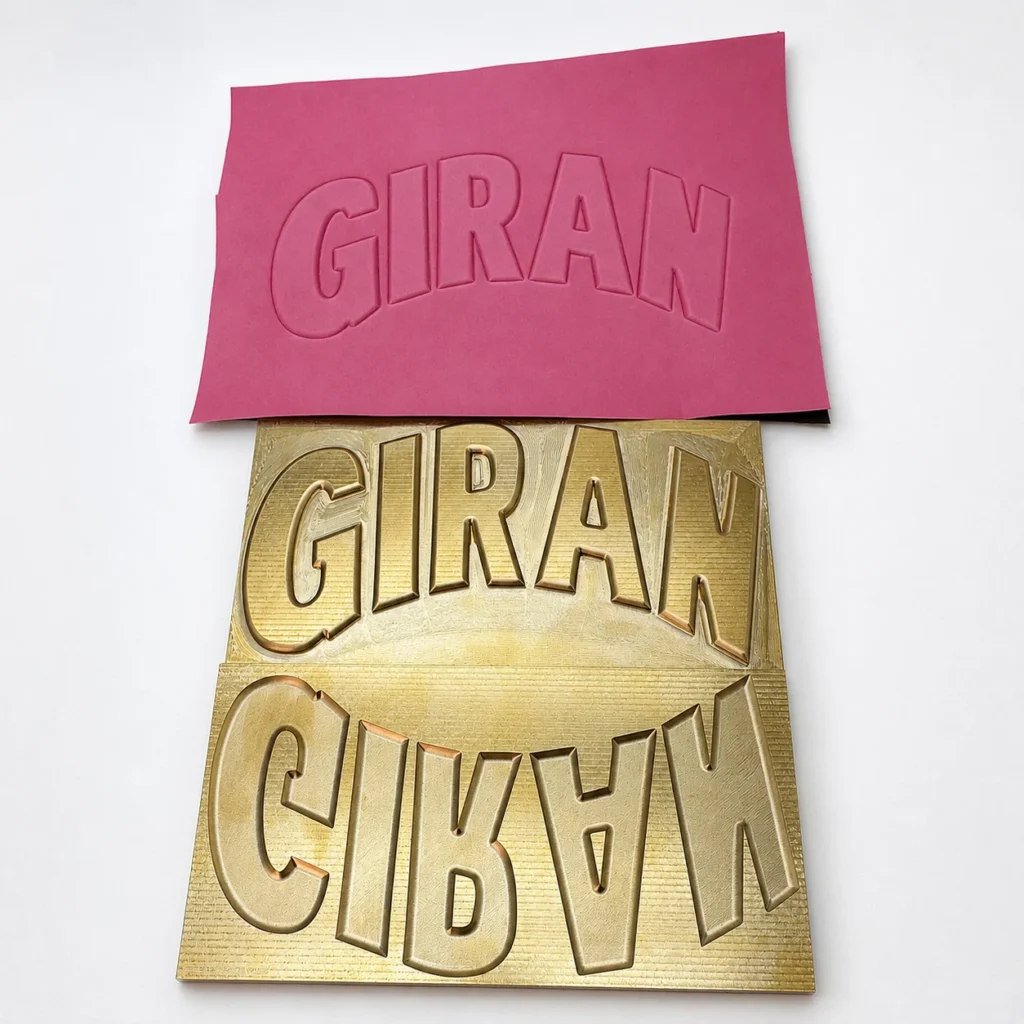
For this test, we used the YTJ-5T 유압식 핫 스탬핑 프레스 together with a 3D relief brass die. If you are building a similar production setup, the die quality matters as much as the machine setting. A well-cut die transfers the depth cleanly and helps the leather release without dragging the texture.
If you need a matching die solution, see 3D 릴리프 황동 핫 스탬핑 다이 and our 포괄적인 워크플로우 솔루션을 위한 승화 인쇄 서비스에 대해 알아보십시오..
The goal of the test was simple:
| 온도 | Embossing Result | Main Risk |
|---|---|---|
| , 호일 전이가 약하고 얼룩이 있었습니다. 110°C에서 | Relief is visible but shallow; fine details are incomplete | Under-forming |
| , PU 표면이 너무 부드러워지고 가장자리가 흐릿해졌습니다. | Clean relief, crisp edges, stable surface, best overall balance | Low |
| 공장 직접 EC-17은 0.01mm 정밀도를 제공하며, 30-50% 더 저렴하고 무료 디자인이 포함되어 있습니다. | Deeper impression, but surface begins to gloss and spread | 중형 |
| 150°C | Strong heat effect, but shrinkage, deformation, and detail loss appear | High |
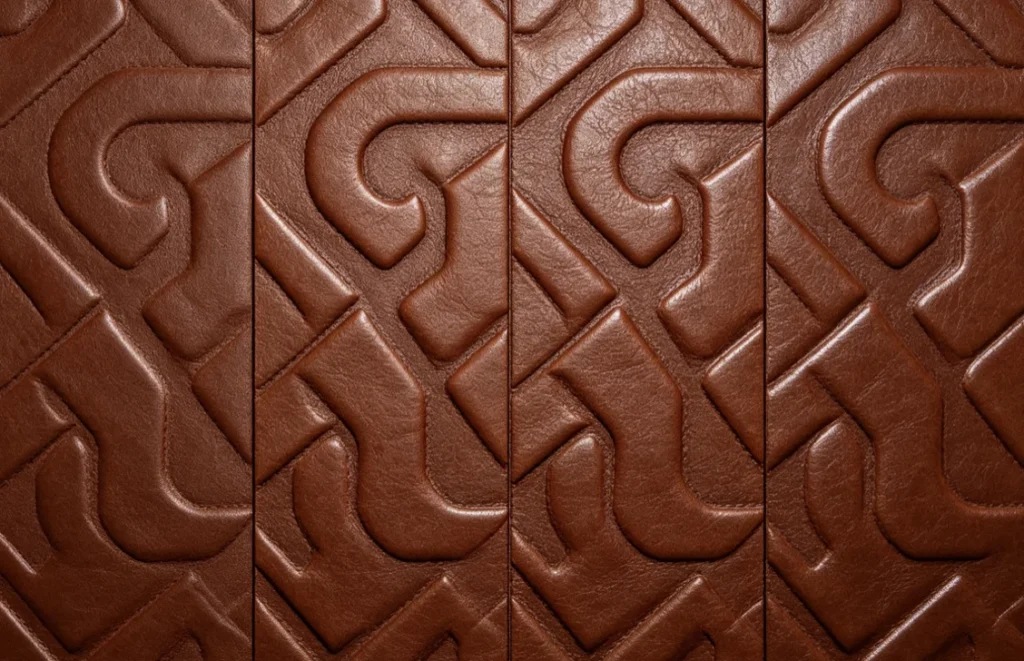
At 90°C, the leather did not fully open up to the die texture. The result looked acceptable from a distance, but the depth was not strong enough for a premium large-area relief effect.
At 110°C, the pattern became much more readable. Edges stayed cleaner, the grain held better, and the embossing looked more controlled.
At 130°C, the relief got deeper, but the leather surface started to show stress. The edges looked softer, and the finish became less natural.
At 150°C, the result moved from embossing into over-processing. The surface lost clarity, and the risk of deformation became too obvious for stable mass production.
110°C hit the middle ground.
It was hot enough to push the leather into the deeper parts of the mold, but not so hot that the grain structure started to collapse. For large-area embossing, that balance is more important than simply chasing the deepest possible impression.
The best result had three qualities:
In other words, 110°C gave us the strongest visual depth without making the leather look overheated.
If you want to reproduce this result, start with a simple test sequence:
The biggest mistake is jumping directly to a high temperature because the first impression looks shallow. Large leather panels can react slowly at first, then suddenly overreact once the heat penetrates.
Practical rule: For large-area leather 3D embossing, improve the result with small adjustments, not big jumps.
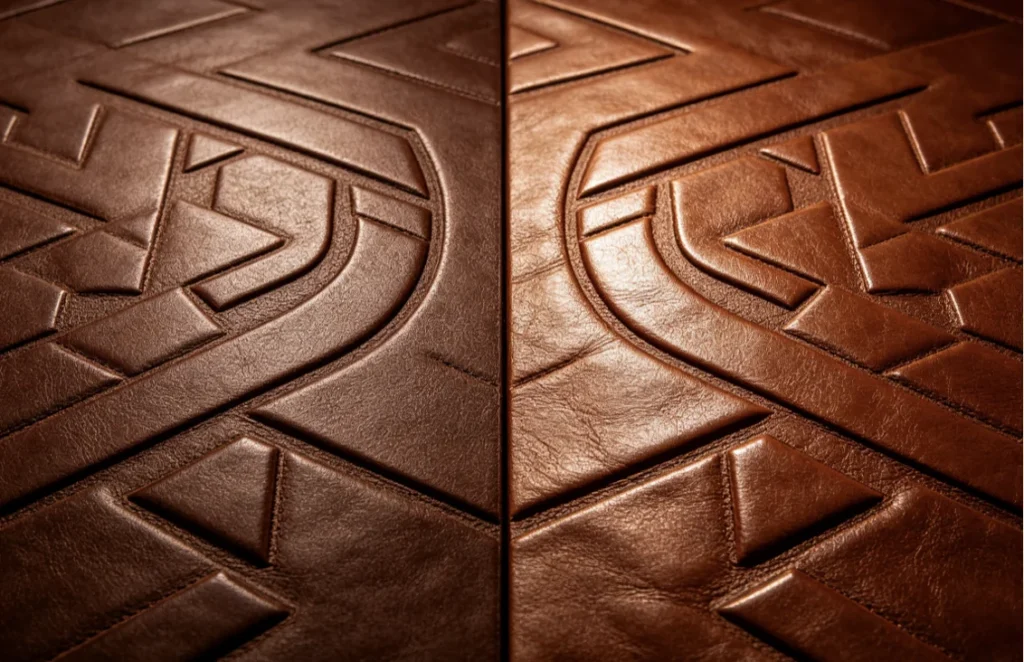
Usually means the temperature is too low, the dwell time is too short, or the die pressure is not fully reaching the surface.
Usually means the temperature is too high or the leather coating is reacting too aggressively.
Usually means the leather is overheating at the boundary area, especially on wide patterns.
Usually means the heat is too strong for the leather grain, or the dwell time is too long.
Usually means the leather thickness or moisture level is uneven, or the machine pressure is not evenly distributed.
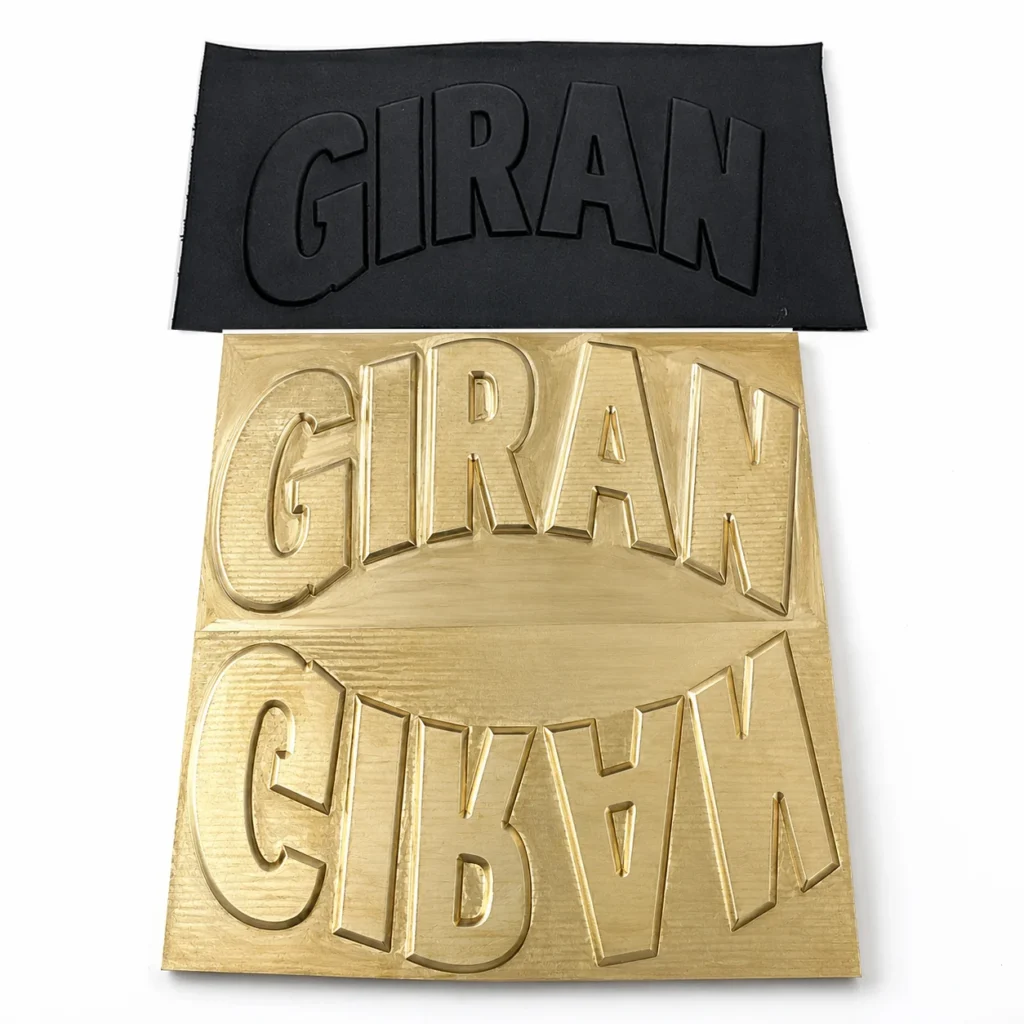
If you are moving from sample testing into production, use the 110°C result as your baseline and then adjust only when the leather type changes.
예를 들어:
Do not assume one setting fits every leather. But do use one stable starting point so your operators are not guessing every time.
If you want a broader machine-selection guide for leather work, read 가죽 제품에 가장 적합한 핫 스탬핑 기계 선택 방법 및 How to Choose the Right Hot Stamping Machine for Leather, Wood and Paper.
This article fits naturally into a leather embossing content cluster. Good internal links include:
In this test, , PU 표면이 너무 부드러워지고 가장자리가 흐릿해졌습니다. gave the best overall result on the YTJ-5T hydraulic hot stamping press. It produced the cleanest balance of depth, edge sharpness, and surface stability.
When the heat is too high, the leather surface layer starts to react more strongly than the inner texture. That can create gloss, flatten the grain, and make the panel look over-processed.
Not safely. Small logos and large relief patterns respond differently because the heat distribution is not the same. Large-area leather usually needs more careful control.
Not always, but for this test it was too aggressive for stable large-area relief. It increased the risk of deformation and detail loss, so it is not a good baseline for production.
Check leather thickness, surface dryness, machine preheat, die alignment, and pressure uniformity. Then run a sample at the lowest practical temperature before scaling up.
For large-area leather 3D embossing, the safest and most useful starting point is 110°C / 2 seconds on the YTJ-5T hydraulic hot stamping press. It gave the cleanest relief in our test and avoided the most common heat-related defects.
If you are producing leather bags, notebook covers, belts, or other premium leather goods, this setting is a strong baseline for sample development. Use it first, then fine-tune only when the leather type or pattern changes.
If you need the matching machine or die, start with the YTJ-5T 유압식 핫 스탬핑 프레스 and the 3D 릴리프 황동 핫 스탬핑 다이.

 English English
 Japanese
 Spanish
 French
 Korean
 German
 Russian