창립자에게 문의하기
아직도 궁금한 점이 있으신가요?
저희 창립자와 직접 연결하세요. 가격이든 기술적인 세부 사항이든 명확한 답변을 받고, 첫 주문을 위한 독점 ‘창립자 보너스’도 받아보세요.
900명 이상의 만족 고객
🏆 1,000건 이상의 맞춤 프로젝트를 성공적으로 납품했습니다.
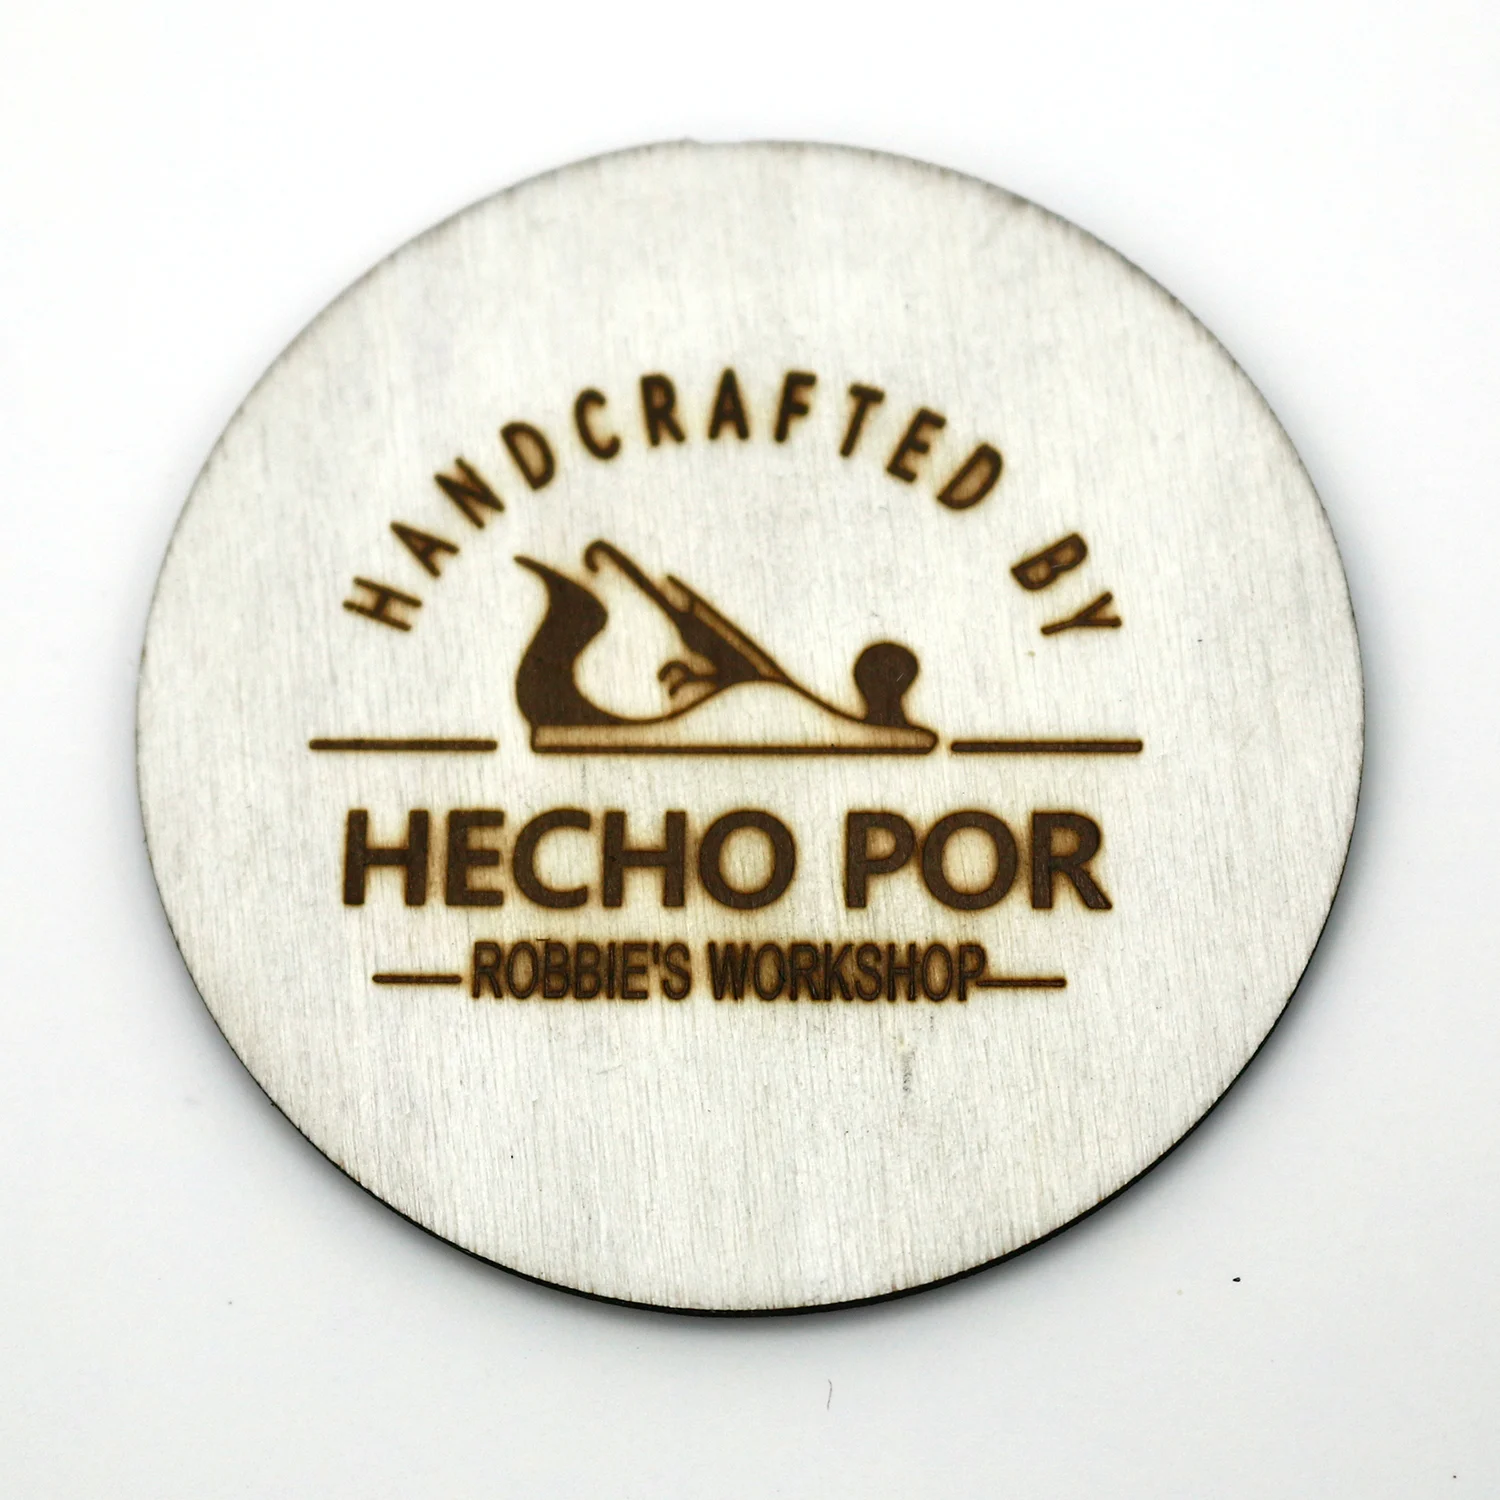
A WT-90DS test compared three temperatures for branding thin wood. 290°C gave the clearest balanced mark, while 350°C caused severe charring.
Thin wood can darken quickly under a heated die. In the supplied WT-90DS comparison, 290°C produced the best overall branding result among 200°C, 290°C, and 350°C: the design and fine lines appeared clearly, the color was moderate, and the sample showed no obvious scorching. The 200°C mark was pale and incomplete, while 350°C caused pronounced charring.
The result applies only to the wood, die, pressure, and dwell time used in the documented test. The report does not identify a wood species, thickness, moisture content, or numeric dwell time, so 290°C should be treated as a sample-test reference rather than a universal setting.
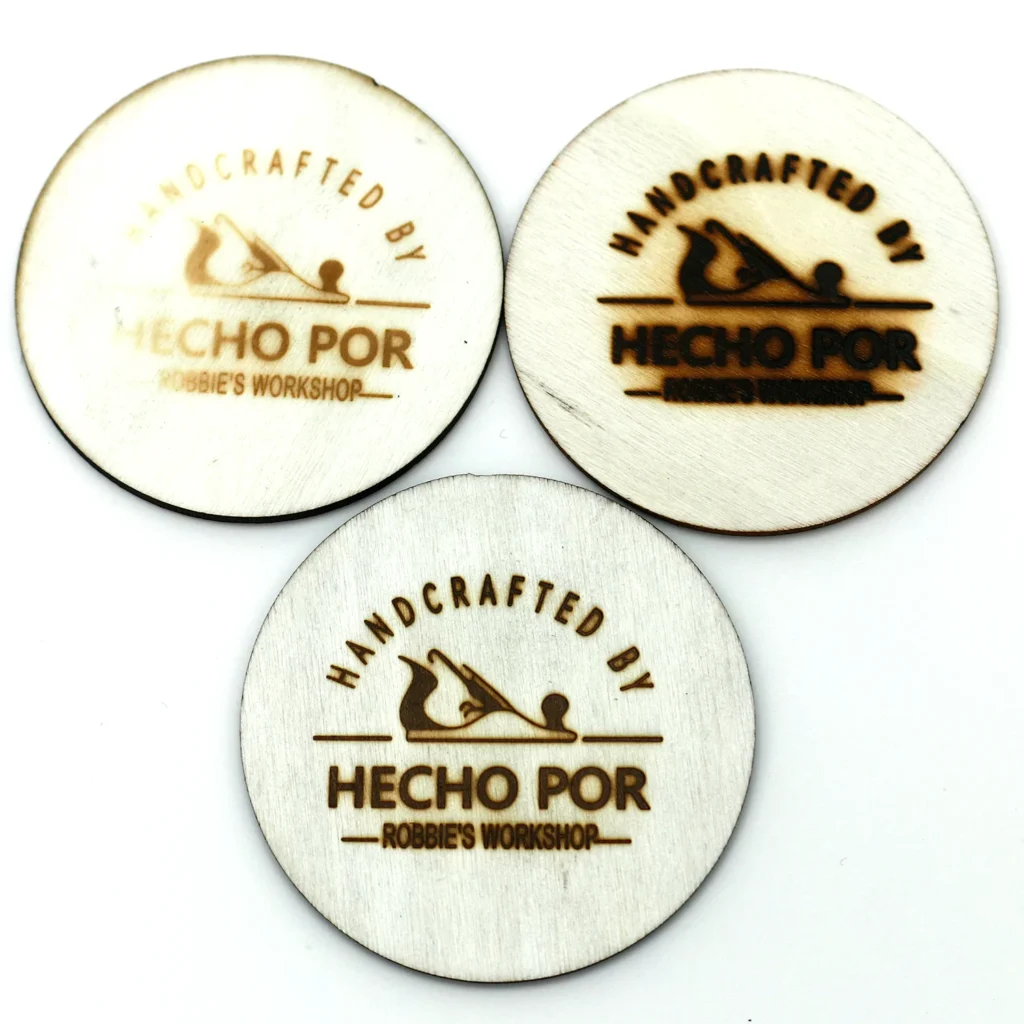
| 온도 | Observed result | Assessment in this test |
|---|---|---|
| 200°C | Pale mark, incomplete areas, and missing fine details | Too low |
| 290°C | Clear and complete design, moderate color, no obvious scorching | Best overall result |
| 350°C | Severe charring, dark heat spread, and loss of detail | Too high |

The 290°C sample showed clear lettering and fine lines without obvious scorching in this test.
The report says other test conditions were kept consistent during the comparison. It identifies 290°C as the recommended reference for the tested thin wood, but instructs users to confirm again when the wood or process changes.
For a repeatable approval, have the supplier review a proof made with the specified stock and die. The FSEA designer’s guide to foil stamping and embossing explains why the selected material and tooling belong in the proof, rather than relying on a temperature number alone.
Thin wood has limited mass to absorb heat from a branding die. The visible mark therefore depends on more than the temperature shown on the controller: species, thickness, moisture, grain direction, surface treatment, die contact, pressure, and dwell time can all affect the result.
This variability is consistent with the USDA Forest Products Laboratory’s Wood Handbook chapter on moisture relations and physical properties, which explains that moisture exchange affects wood properties and performance. The report does not identify the tested wood species or moisture content, so neither the 290°C reference nor this sample should be generalized to every wood product.
At insufficient heat, the design may look faint or incomplete. At excessive heat, the wood fibers can char and the darkened area can spread beyond the intended lines. A useful test must evaluate both mark visibility and the surrounding wood surface.
이 WT-90DS Manual Hot Stamping Machine for Thin Wood Branding was evaluated at three temperatures. The test focused on design completeness, edge clarity, color, scorching, and production suitability. If you are still deciding between a heated branding mark, foil transfer, or a raised impression, first compare the process differences in this guide to embossing, foil stamping, and heat branding.
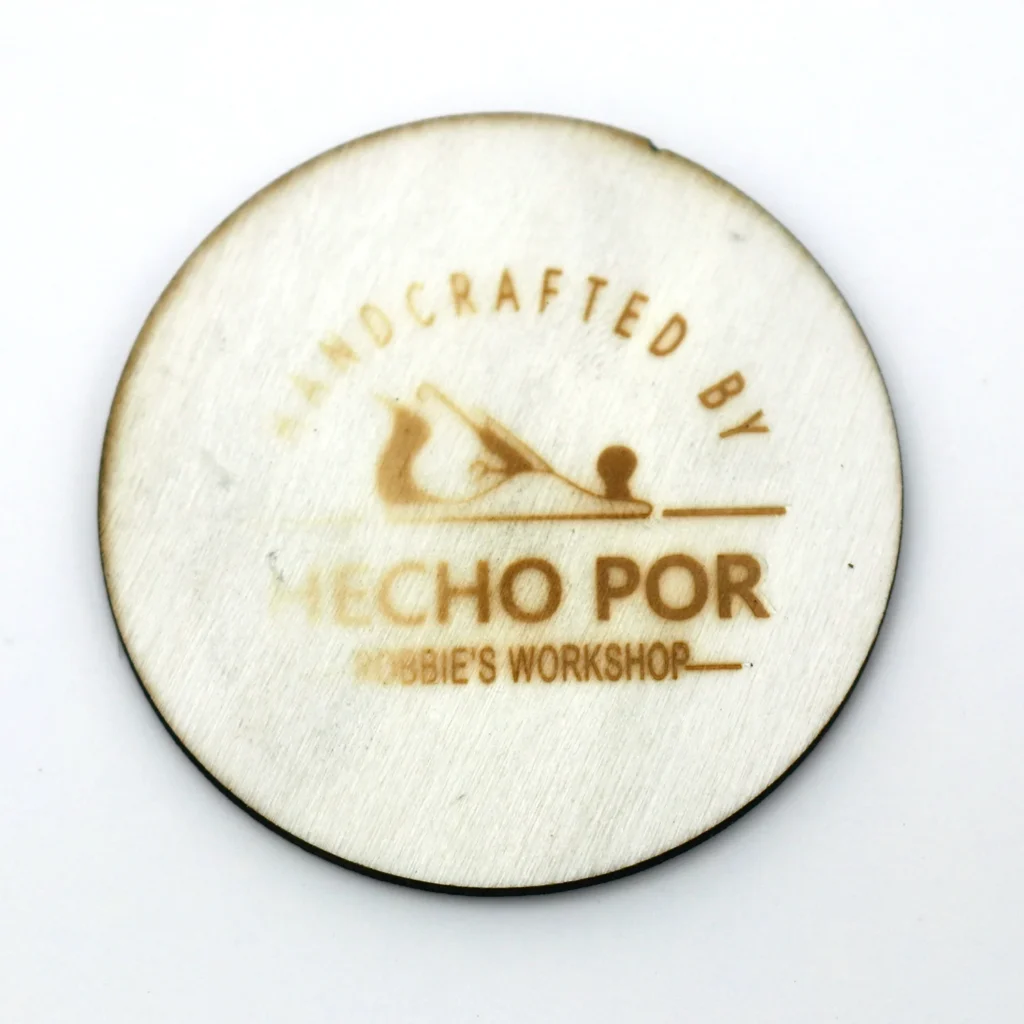
At 200°C, the die did not produce enough visible heat reaction for the tested setup. Parts of the curved lettering, the left side of the design, and lower text were faint or missing. Fine lines and small letters were not stable enough for the report’s production criteria.
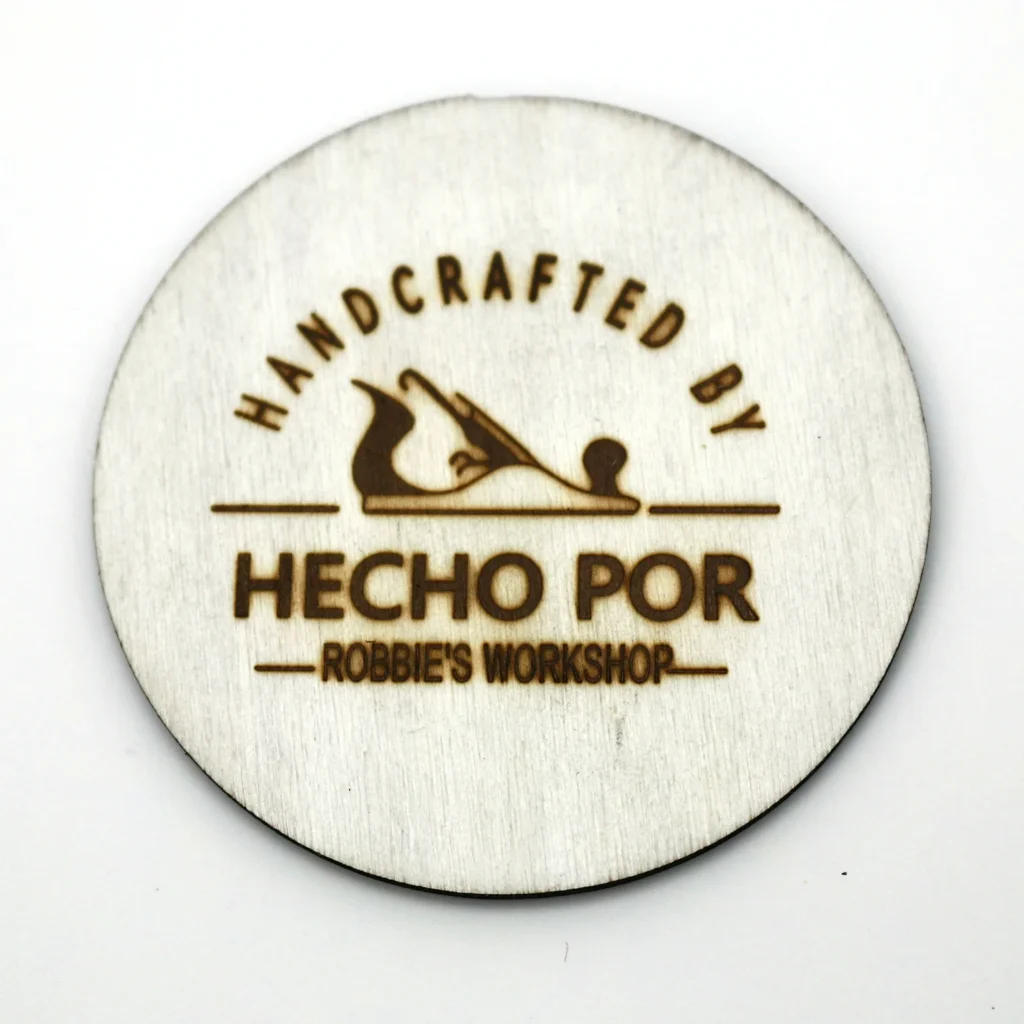
At 290°C, the main artwork, lettering, and fine lines were clearly visible. The mark had moderate, even color and reasonably clean edges, while the wood showed no obvious blackening or broad heat discoloration. The report therefore identifies 290°C as its production reference for the tested setup.
At 350°C, the design area became heavily carbonized, with dark brown-to-black heat spread around the mark. The edges appeared heavier, and charring obscured some visual layers and fine detail. The report judged this setting unsuitable for the tested production requirement.
Start near the tested 290°C only if your wood and tooling are reasonably comparable. Hold pressure, dwell time, die, workpiece thickness, and placement steady during initial comparisons so that one change can be evaluated at a time. If a mark is pale, first verify flat contact and alignment before raising temperature substantially.
For a new material, document the species, thickness, moisture condition, surface finish, die artwork, temperature, and press duration. Allow for heat build-up during repeated cycles, inspect samples periodically, and clean residue from the die. Repeat the test when the wood batch, coating, die, or production rhythm changes.
For custom logo tooling, review the brass branding iron options 및 custom brass stamps for wood and leather; ask the supplier to confirm mounting and heating compatibility with the WT-90DS before ordering. If you are choosing a press as well as a die, the hot stamping machine selection guide can help structure that decision.
The supplied test found 290°C to be the best of its three settings: 200°C, 290°C, and 350°C. This reference applies to the tested sample and process, not all wood species or thicknesses.
The report describes insufficient heat reaction: parts of the design and fine details were faint or missing. Check contact, alignment, pressure, and dwell time as well as temperature when validating a new job.
The wood showed severe charring and dark heat spread. The heavier dark areas also reduced the visibility of fine details, so the report did not recommend 350°C for this setup.
No. Wood species, thickness, moisture, grain, surface treatment, die geometry, pressure, and dwell time can all change the result. Run a sample on the actual material before production.
In the documented WT-90DS thin-wood branding test, 290°C gave the clearest balanced mark. At 200°C, parts of the design remained pale or incomplete; at 350°C, charring became excessive. Use 290°C as a reference for a comparable setup and validate each new wood batch with a controlled sample.
See the WT-90DS product page for machine details, and contact ZHENGFEI with your wood sample, thickness, artwork, and target mark before production.

 English English
 Japanese
 Spanish
 French
 Korean
 German
 Russian