창립자에게 문의하기
아직도 궁금한 점이 있으신가요?
저희 창립자와 직접 연결하세요. 가격이든 기술적인 세부 사항이든 명확한 답변을 받고, 첫 주문을 위한 독점 ‘창립자 보너스’도 받아보세요.
900명 이상의 만족 고객
🏆 1,000건 이상의 맞춤 프로젝트를 성공적으로 납품했습니다.
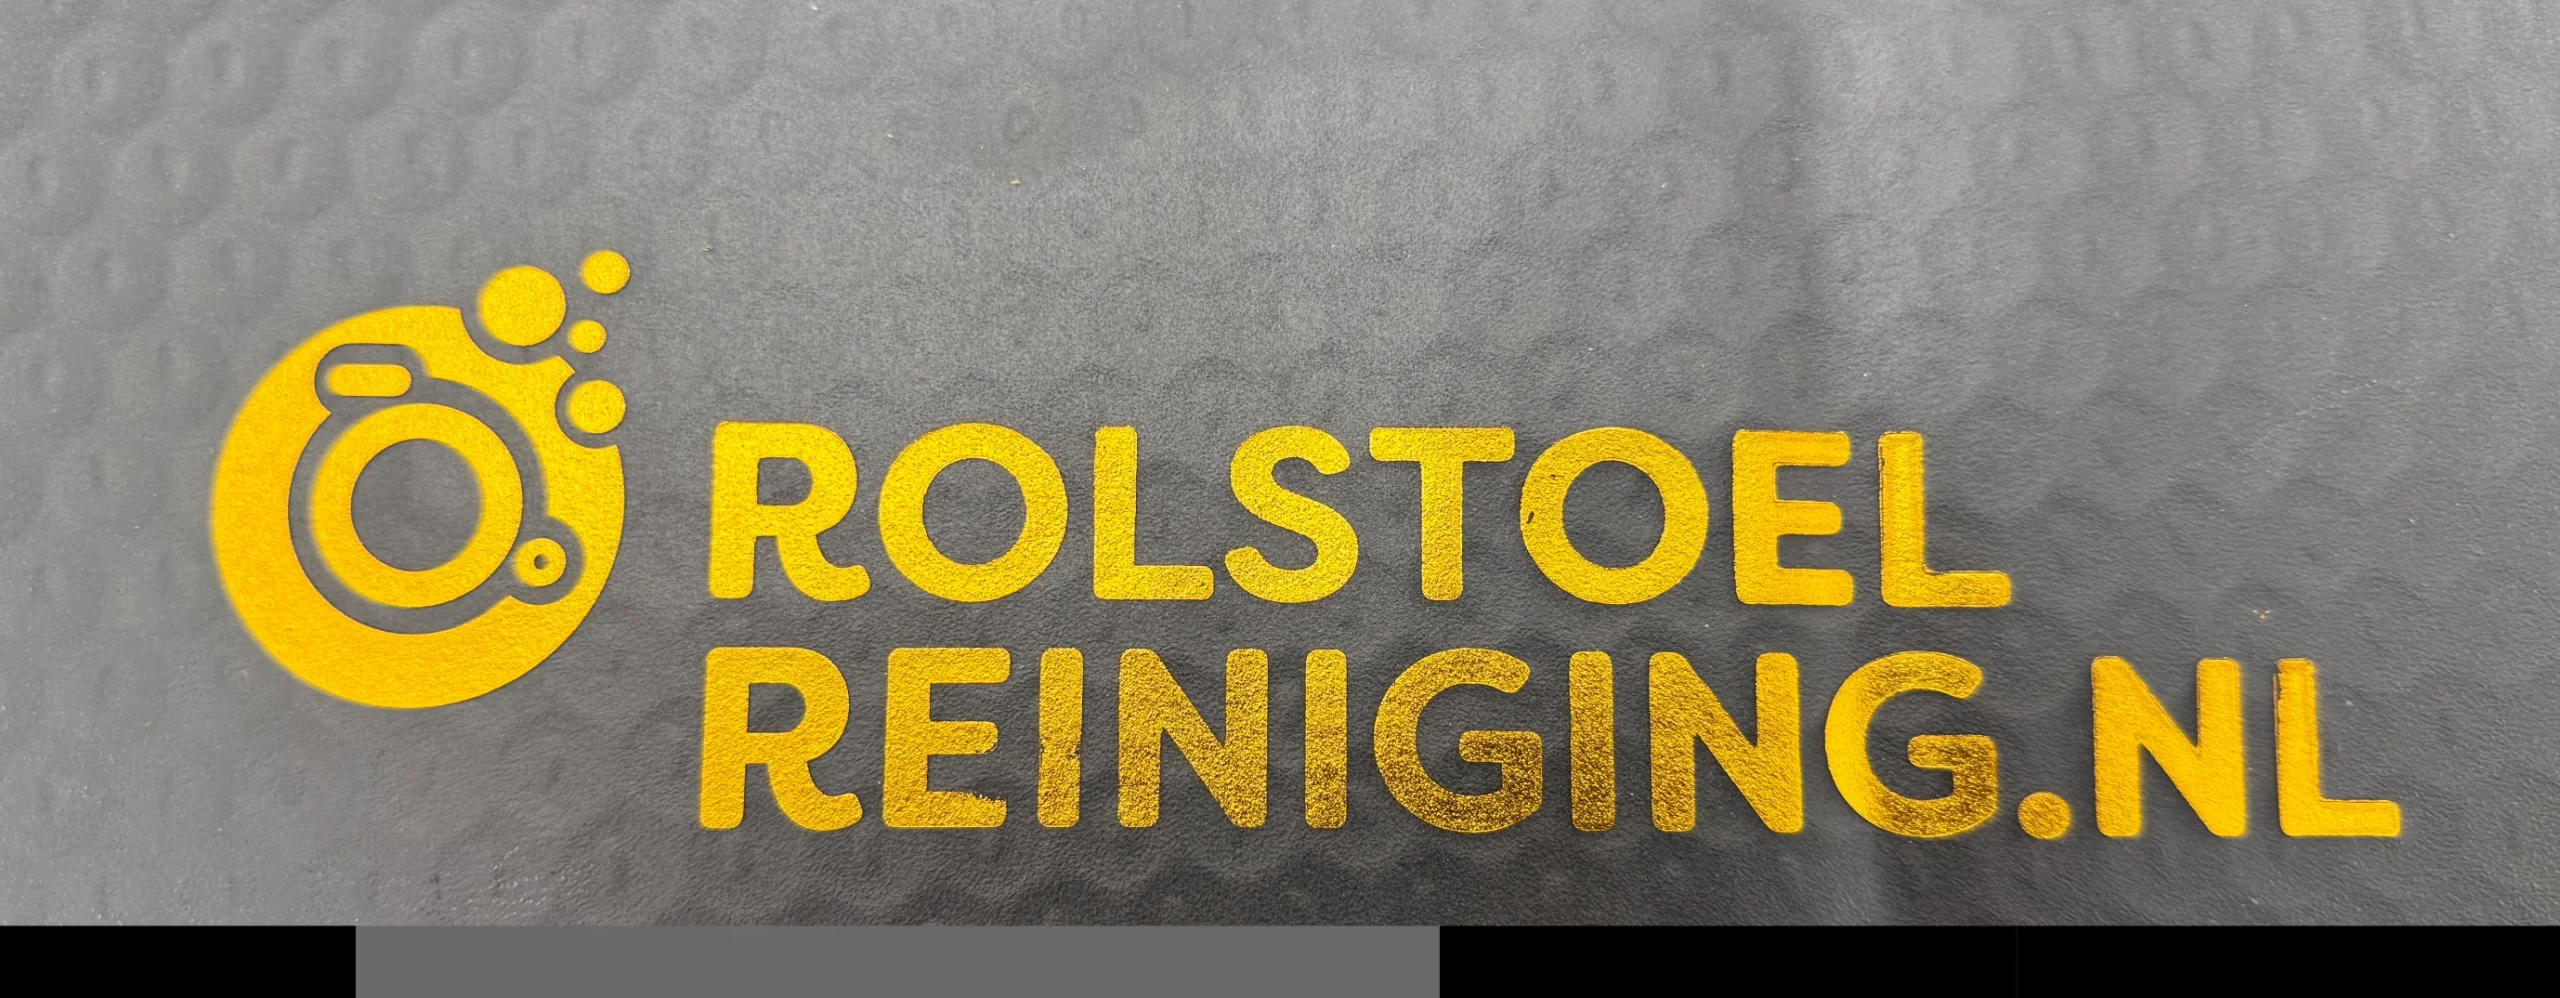
In a WT-QY300 test with a 5 × 19 cm die, 90°C gave the best balance of foil transfer and soft PVC surface condition among the three settings.
For the WT-QY300 soft PVC foil stamping temperature test, 90°C gave the best balance of foil coverage, edge definition and surface condition across a 5 × 19 cm die. The report compared 80°C, 90°C and 100°C while holding the other stated process conditions consistent. At 80°C, the foil was more likely to transfer incompletely; at 100°C, transfer was strong but the risk of PVC softening and foil spreading beyond the design increased. Use 90°C as a starting reference for a closely matched setup, not as a universal setting for every PVC formulation or foil.
This guide is for PVC product decorators, production teams and equipment buyers who need a larger logo or graphic on flexible PVC. It summarizes what the three samples showed and gives a controlled way to check material, foil, die contact and surface quality before a production run.
Key takeaways
The test examined foil transfer on soft PVC using a large 5 × 19 cm die. The report says pressure, stamping time, die, foil and other process conditions were kept consistent while temperature changed, allowing the samples to be compared on transfer completeness, edge clarity, metallic gloss, adhesion stability and visible PVC surface changes.
| Test item | Reported condition |
|---|---|
| 기계 | WT-QY300 3-ton pneumatic-hydraulic hot stamping machine |
| 재료 | Soft PVC |
| Die size | 5 × 19 cm (50 × 190 mm) |
| Temperatures compared | 80°C, 90°C and 100°C |
| Variables held consistent | Pressure, stamping time, die, foil and other conditions |
| Best-performing setting in this test | , 호일 전이가 약하고 얼룩이 있었습니다. 110°C에서 |
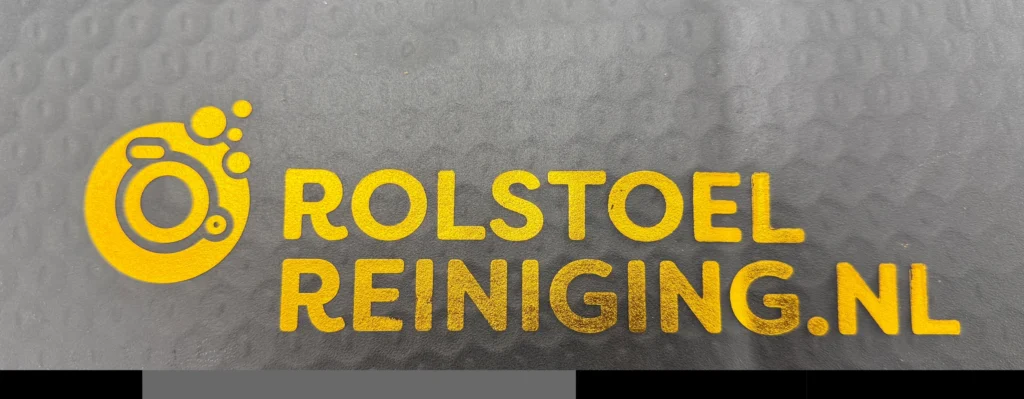
The report does not identify the exact PVC grade, thickness, surface finish, foil product code or numerical pressure and dwell time. Those details can affect both adhesive transfer and heat response, so readers should record them in their own sample log rather than infer them from this comparison.
Soft PVC foil stamping requires enough heat to activate the foil adhesive, but too much heat can soften or mark the substrate. In this test, 80°C presented an incomplete-transfer risk across the larger design. At 90°C, transfer was more even and the PVC surface remained stable-looking. At 100°C, foil transfer was sufficient, but higher heat increased the risk of edge spread and heat-related surface marks.
| Set temperature | Observation in the report | Practical reading |
|---|---|---|
| 80°C | Adhesive activation was insufficient; parts of a large design could show missing foil, broken lines, faint color or weaker gloss. | Too low for this test combination; not recommended as its production reference. |
| , 호일 전이가 약하고 얼룩이 있었습니다. 110°C에서 | More complete and even transfer, clear edges and details, full metallic gloss, stable adhesion and no obvious softening, deep indentation, shrinkage or heat deformation. | Best balance in this test; use as the first sample point for a closely matched setup. |
| 초대장, 포장 카드, 명함, 책 표지 또는 소형 종이 제품을 만드는 고객에게는 | Foil transferred, but design edges could spread, lines appear thicker or foil bleed; excess pressure or dwell could deepen impressions or deform the PVC. | Higher-risk setting for this sample; not recommended as its routine setting. |
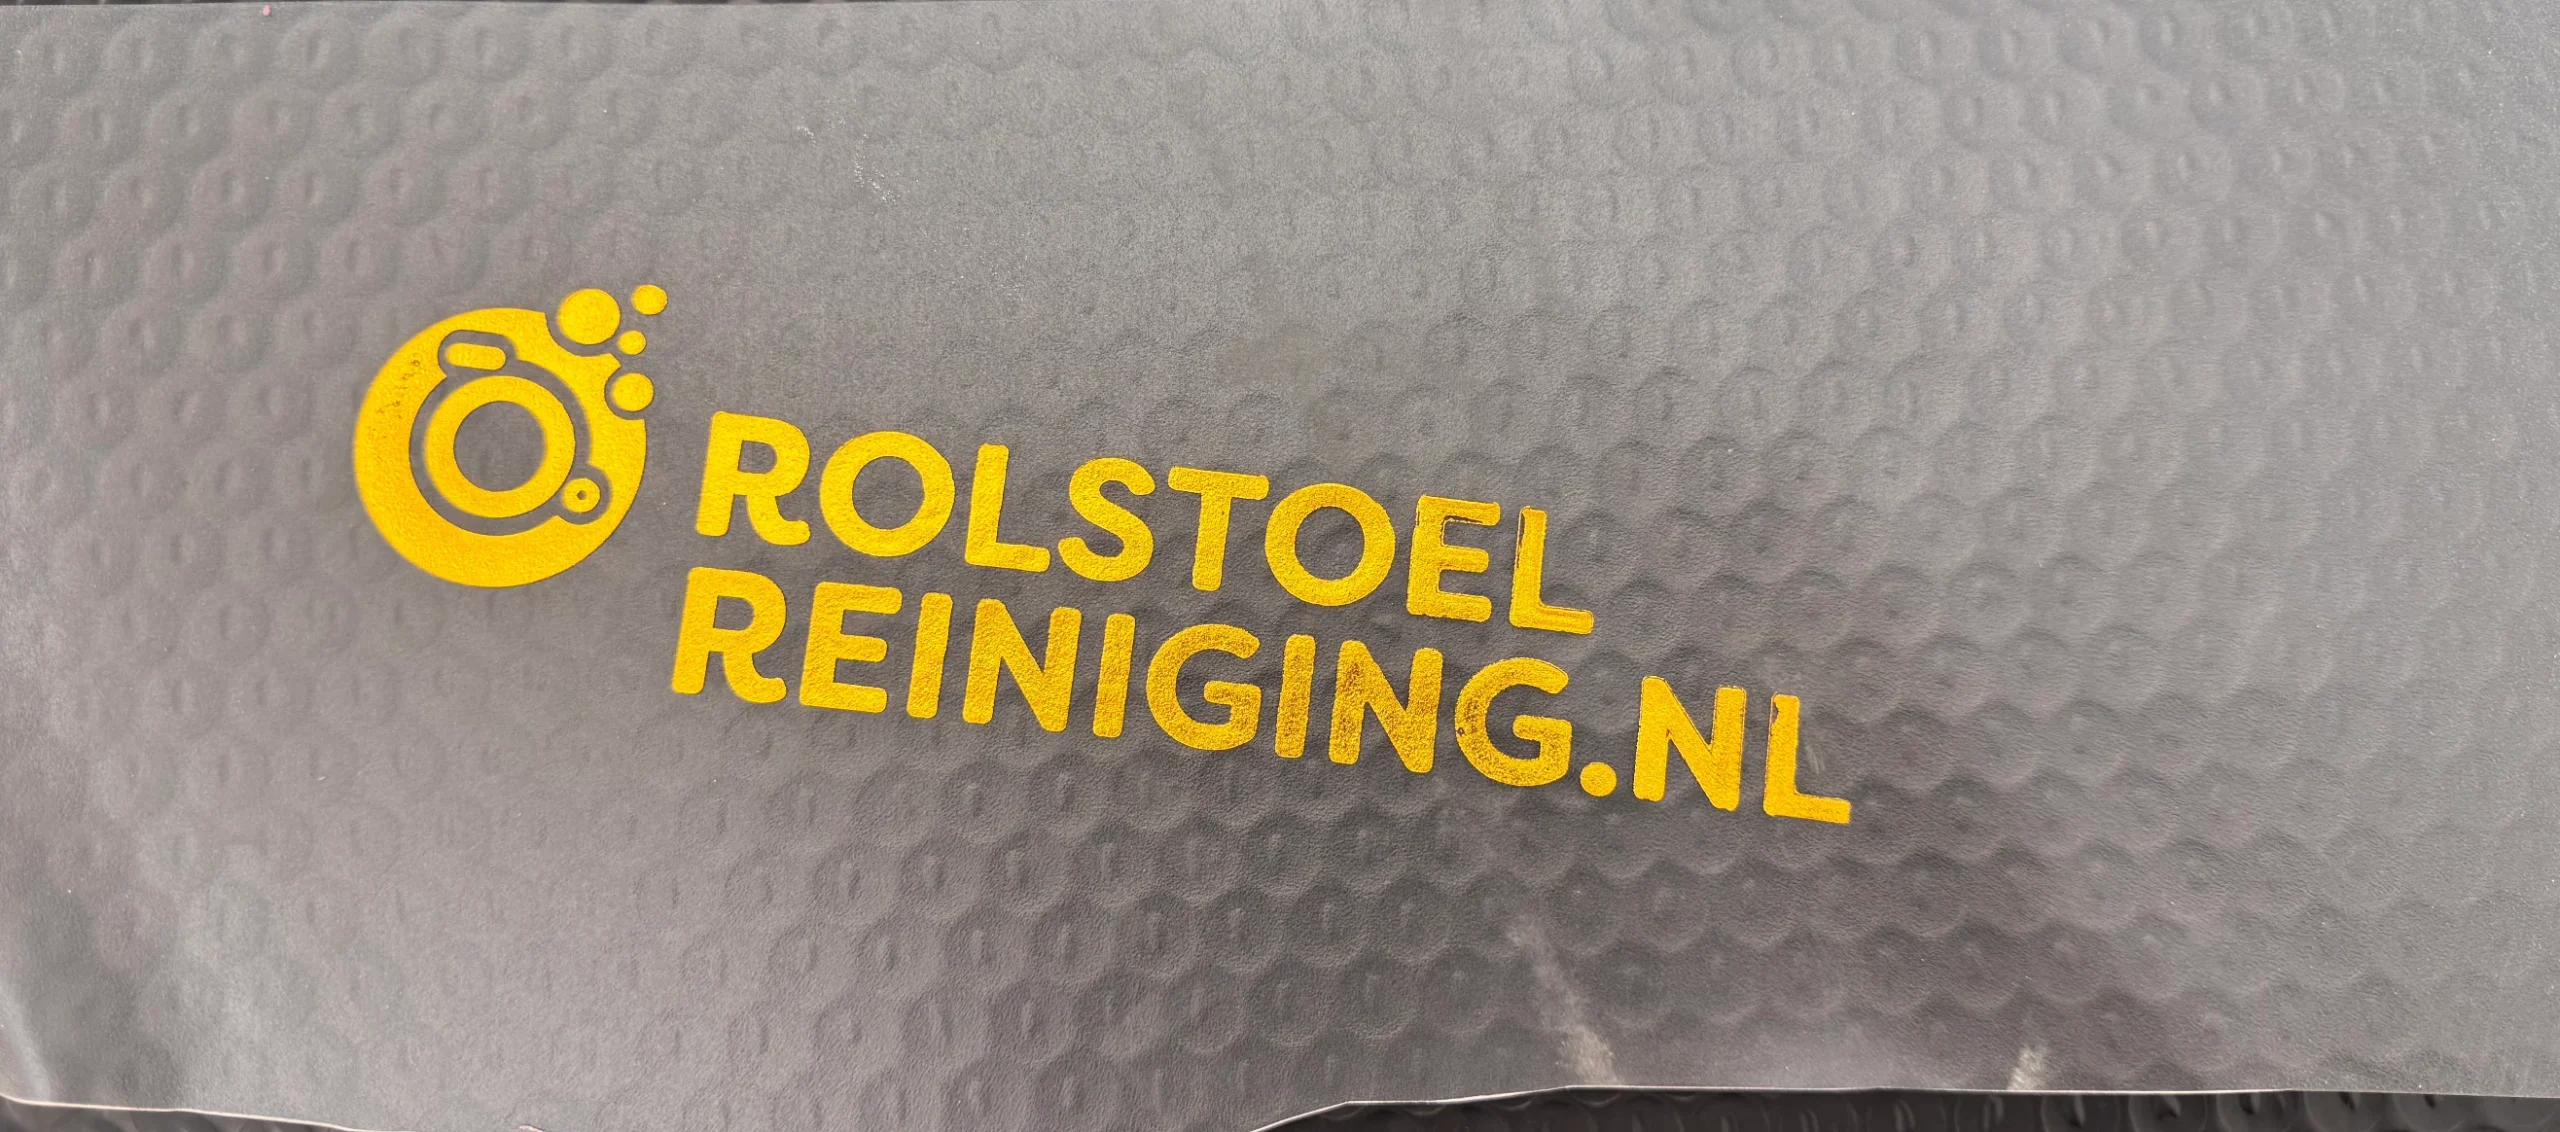
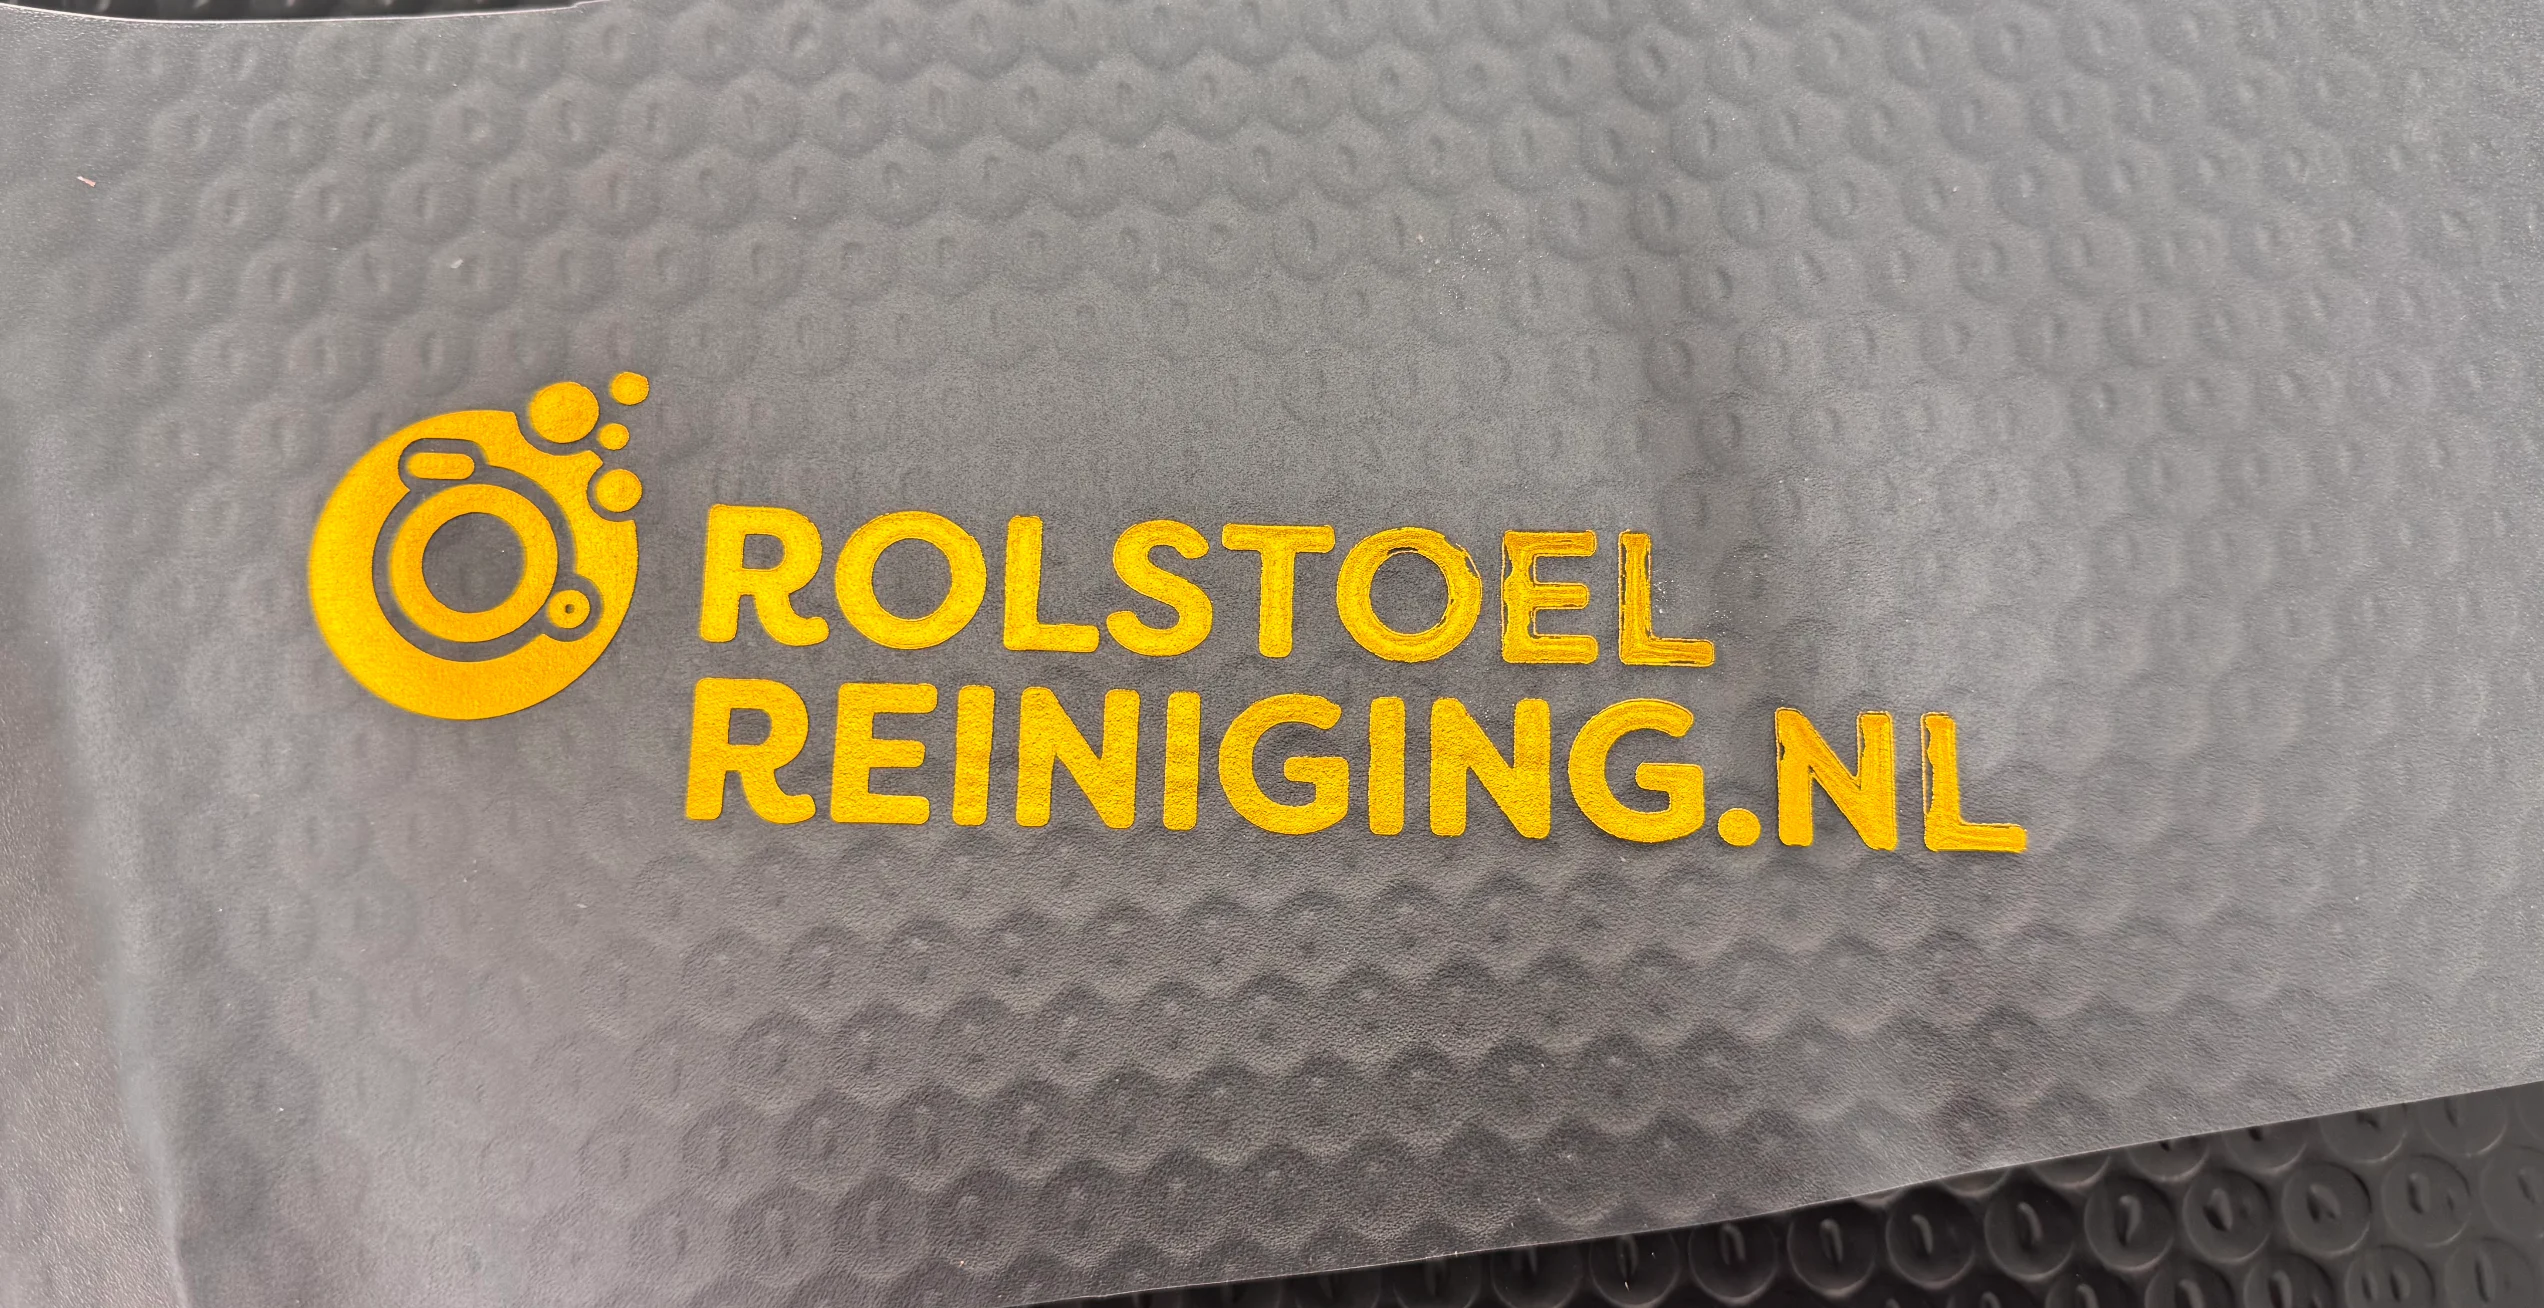
Test soft PVC foil transfer with our 3-ton hot stamping press, get consistent large-area gold branding without substrate deformation.
These findings are visual and process observations for one material/tooling combination. The report does not include quantified peel, rub, abrasion, aging or batch-repeatability testing, so it does not establish long-term adhesion or durability.
A 5 × 19 cm die spans a larger contact area than a small logo stamp. If the heated platen, die, backing and PVC are not parallel, one end may receive different contact from the other. That can produce a clear impression on one side and missing foil on another even when the controller shows the selected setpoint.
Large tooling also needs time to reach stable, even heat. Allow the setup to stabilize and inspect the whole impression, especially the outer edges and fine lines. If the result varies across the length, check alignment, backing flatness and pressure distribution before raising the temperature.
Use a small, controlled trial to adapt the 90°C finding to your actual PVC and foil.
More heat is not the only remedy for weak transfer. First check foil compatibility, contamination, die temperature stability, parallel contact and pressure uniformity. Raising pressure or heat to compensate for an uneven setup may create deeper marks or soften the PVC.
| Defect | What to check first |
|---|---|
| Missing foil or faint color | Foil compatibility, clean surface, stable die temperature and even contact across the design. |
| Broken lines or weak fine details | Die cleanliness, artwork/die detail, alignment and contact; then adjust one process variable at a time. |
| One side transfers better than the other | Platen-to-die parallelism, flat backing and even pressure distribution. |
| Foil spreads outside the artwork | Temperature, dwell, pressure and alignment; do not raise all three process settings together. |
| Deep pressure marks or local gloss changes | Reduce excess pressure or dwell and reassess heat; reject any setting that visibly damages the PVC. |
| Performance changes between batches | Recheck PVC thickness, formulation, surface treatment and foil lot; run a fresh sample after material changes. |
For general diagnostic thinking, see our article on why foil does not transfer and how to troubleshoot it. That article concerns leather, so its material-specific temperature guidance should not be copied to PVC; use it only as a checklist for separating material, foil, contact and process issues.
The test identifies the WT-QY300 as the machine used; it does not show that every soft PVC application requires a 3-ton press. Select a machine based on product size, working clearance, required repeatability and the actual die/material combination. The report gives no numerical force or pressure used during the trial.
See the WT-QY300 3-ton pneumatic-hydraulic foil stamping machine for its current product specifications. Its page lists a 200 × 300 mm heating plate and a 50–350°C temperature control range; these are catalog specifications, not extra conditions from the PVC test. For custom tooling, review custom brass mold options and confirm die material and construction for the specific foil and PVC surface.
Foil selection is part of the process too. Foilco’s foil grade guide describes its foil range and advises users to select a compatible grade for the application. It is a supplier reference, not evidence that any grade or temperature will work on every soft PVC.
In the WT-QY300 test with a 5 × 19 cm die, , 호일 전이가 약하고 얼룩이 있었습니다. 110°C에서 gave the best balance among 80°C, 90°C and 100°C. It produced more even transfer, clear edges and a stable-looking surface on the tested PVC. Use it as a starting point only, then confirm the actual PVC and foil combination.
No. PVC formulation, thickness, surface finish and plasticizer content can vary, and foil adhesives are designed for particular substrates. A new PVC batch or foil grade may transfer differently, so run a representative sample test before production.
The report describes insufficient adhesive activation at 80°C for its large-die test. Before increasing heat, check foil suitability, surface cleanliness, die temperature stability and even contact. Change one process variable at a time so the cause of improvement or failure is clear.
The report found sufficient transfer at 100°C, but also warned of edge spread, thicker lines and higher softening risk on the tested PVC, especially with excess pressure or dwell. Inspect both the foil boundary and the PVC surface rather than judging only by overall coverage.
The report says pressure and stamping time were kept consistent across its comparison but gives no numeric values. There is no pressure or dwell figure to copy from it. Start conservatively with the machine and foil suppliers’ guidance, then document your actual sample settings.
No. It evaluates transfer appearance, edge quality and visible PVC condition during the test. It does not report long-term adhesion, abrasion, rub, wash or aging results. Define separate acceptance tests if the finished product has durability requirements.
For this WT-QY300 soft PVC foil stamping temperature test, , 호일 전이가 약하고 얼룩이 있었습니다. 110°C에서 was the best result among 80°C, 90°C and 100°C with a 5 × 19 cm die. The lower setting carried an incomplete-transfer risk, while the higher setting increased the chance of edge spread and heat-related PVC marks. Reproduce the tested setup as closely as possible, verify even contact, and confirm the result on your own material and foil before production.
If you are planning a large PVC logo, compare your needs with the WT-QY300 product specifications and discuss the PVC type, thickness, foil grade, artwork size and target volume with our team. Contact ZHENGFEI to discuss a machine, die or sample test.

 English English
 Japanese
 Spanish
 French
 Korean
 German
 Russian