창립자에게 문의하기
아직도 궁금한 점이 있으신가요?
저희 창립자와 직접 연결하세요. 가격이든 기술적인 세부 사항이든 명확한 답변을 받고, 첫 주문을 위한 독점 ‘창립자 보너스’도 받아보세요.
900명 이상의 만족 고객
🏆 1,000건 이상의 맞춤 프로젝트를 성공적으로 납품했습니다.
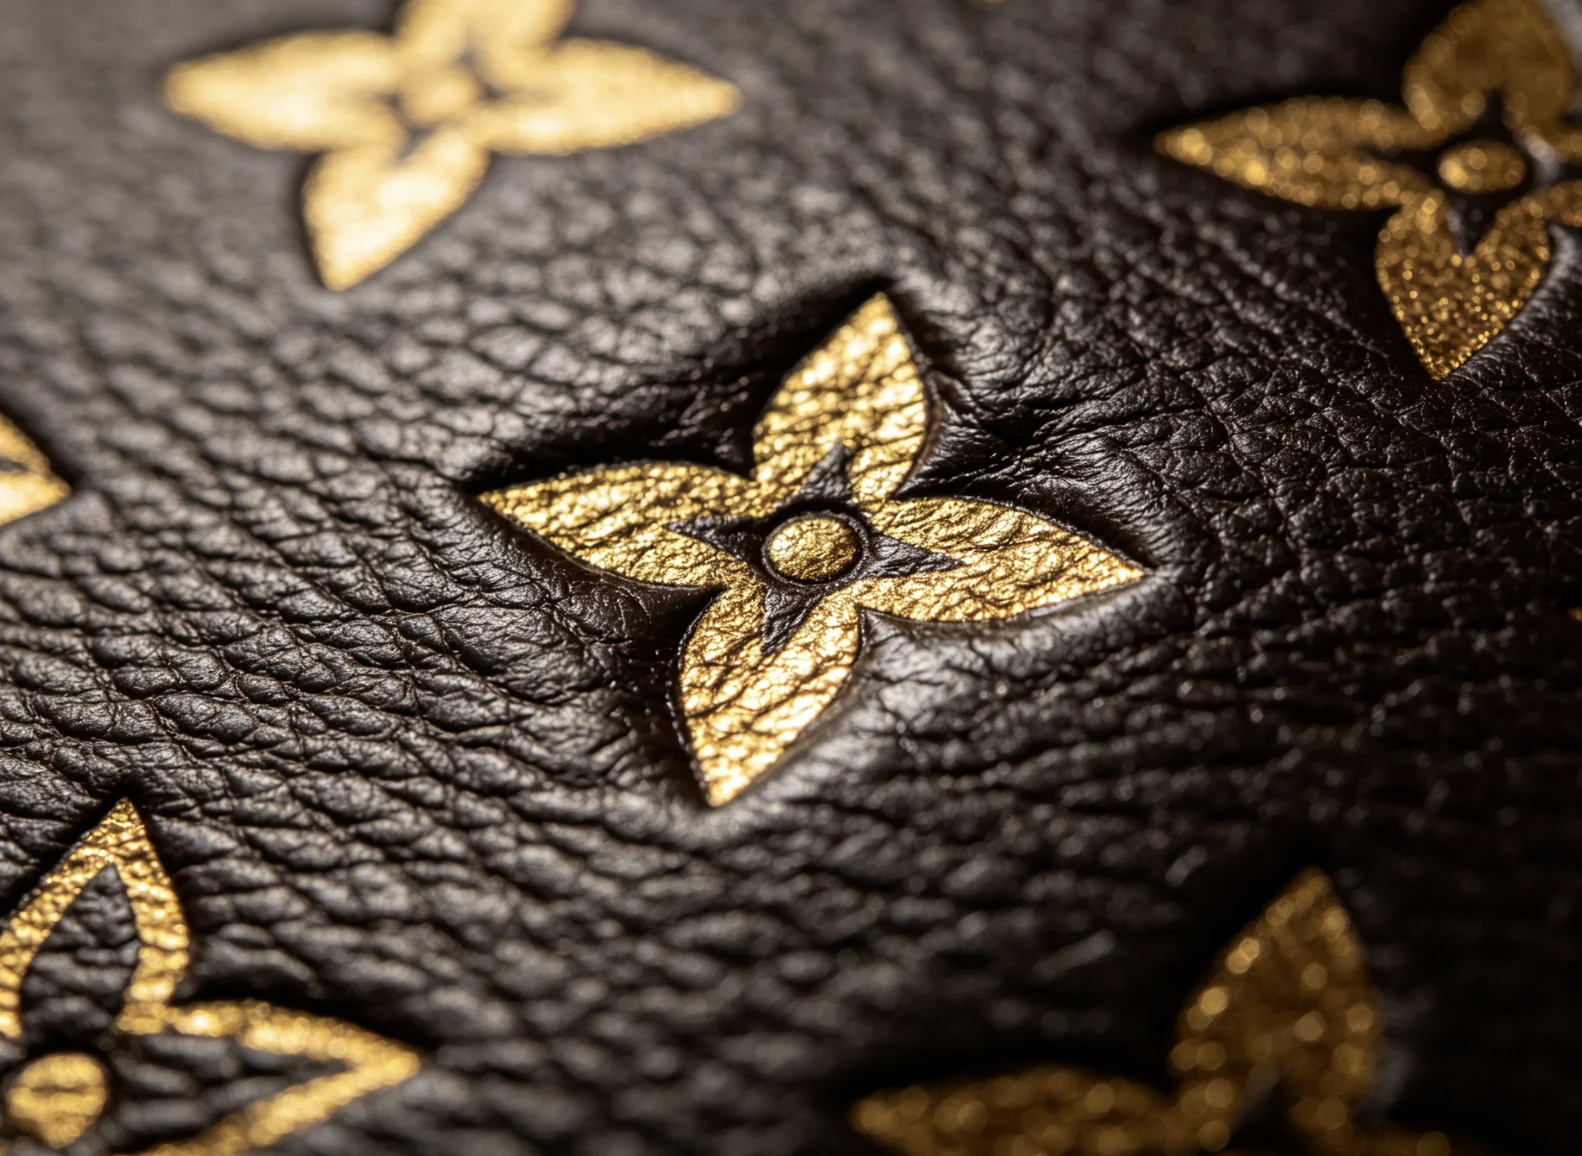
Hot stamping leaves deep marks on leather when the process is too aggressive for the material. The usual causes are too much pressure, too high temperature, too long dwell time, a large solid die area, soft leather, weak material support, or a die that is not level.
For clean leather foil stamping, aim for enough heat and pressure to transfer the foil, but not so much that the die sinks deeply into the leather. A shallow, even impression is usually better than a deep mark when the goal is metallic foil. Test on scrap leather first, reduce one variable at a time, and match the die size and machine to the material.
Not every pressed mark is a defect. Some customers want a blind debossed logo or a deeper branded look. The problem starts when the mark is deeper than expected, the surrounding leather becomes shiny, the surface wrinkles, the logo edge spreads, or the material coating is damaged.
Use this quick distinction:
| Result | What It Looks Like | Is It a Problem? |
|---|---|---|
| Clean foil stamp | metallic foil transfers with a slight impression | usually ideal |
| Light deboss with foil | foil sits in a shallow pressed mark | acceptable for many leather goods |
| Deep deboss | logo is clearly sunken without tearing or deformation | good only if intentional |
| Shiny pressure mark | smooth glossy area appears around the logo | usually a process problem |
| Fuzzy or spread edge | foil and leather edge blur outward | too much heat, pressure or dwell time |
| Wrinkled or sunken leather | material surface changes shape around the die | material damage |
| Scorch or melted coating | dark, burned, sticky or hardened surface | serious overheating |
If the foil itself is missing or weak, start with 왜 포일이 가죽에 전이되지 않으며 이를 고치는 방법. If the issue is extra gold around the design, read 스탬프 주변에 금박 포일이 더 묻어나는 이유는 무엇인가요?.
Leather is not a flat plastic sheet. It has thickness, grain, coating, softness and memory. When a heated die presses into it, the leather responds to both mechanical pressure and heat.
Deep marks happen when the die pushes too far into the surface or when heat softens the leather enough for the die to sink. On PU leather, the coating can soften or deform. On genuine leather, the grain can flatten, darken or become shiny. On soft leather goods, the whole product may compress unevenly.
This is why a setting that works on one leather sample may damage another.
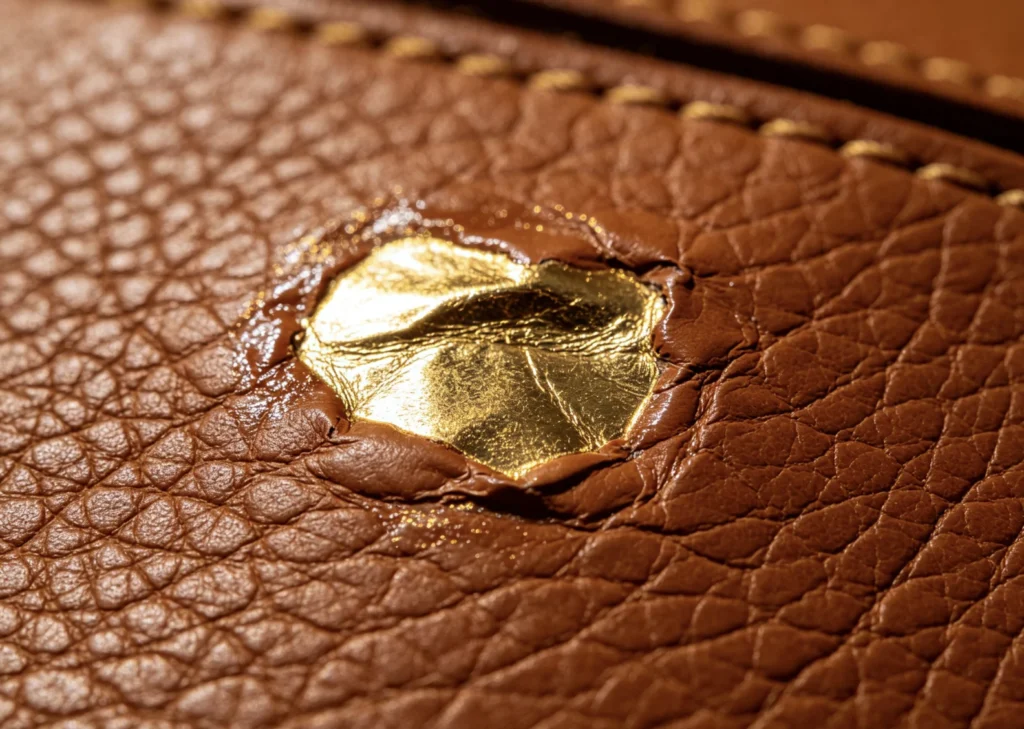
Pressure is necessary for foil transfer, but more pressure does not always create a better stamp.
If pressure is too strong, you may see:
This is common when users try to solve weak foil transfer by pressing harder. If the real problem is low temperature, wrong foil or poor die contact, extra pressure may only damage the leather.
For foil stamping, the die should usually press just enough to create contact and transfer. For a deliberate blind deboss, a deeper mark can be acceptable, but it should be planned as the final effect, not created accidentally.
High temperature can soften leather coatings and make pressure marks worse. On PU leather especially, heat can make the surface easier to dent, blur or deform.
Based on Zhengfei workshop tests, EC-27 letter type and QS201 brass die work on tested PU leather gave clean results around 100°C with short dwell time. At higher temperatures, the metallic effect could look stronger, but small text was more likely to show edge spread. Around 120°C in the test notes, PU leather could soften, show press marks or produce fuzzy edges.
For 90XTS thick letter type on tested PU leather, around 110°C with 1 second was a strong reference. At higher temperatures, edge spread and material stress became more likely.
These are reference settings, not universal rules. The exact value depends on PU coating, genuine leather type, foil model, die size, pressure, dwell time and artwork detail.
Dwell time is how long the heated die stays in contact with the material. A longer dwell gives more time for foil adhesive activation, but it also gives more time for heat to move into the leather.
Too much dwell time can cause:
If the foil transfers but the leather is damaged, shorten dwell time before increasing pressure. For small letters and fine logos, short dwell time often gives cleaner edges.
A small logo and a large solid block do not behave the same.
Large dies need more even pressure across the full surface. If the machine, material support or die mounting is not stable, one area may stamp cleanly while another area presses too deeply.
Large solid designs are more likely to create:
Before engraving a large logo, review the artwork. Sometimes changing a solid logo into an outline, reducing filled areas or increasing line spacing can make the stamping result cleaner.
For design limits, read 황동 포일 스탬프는 얼마나 넓은 실면적을 가질 수 있나요?.
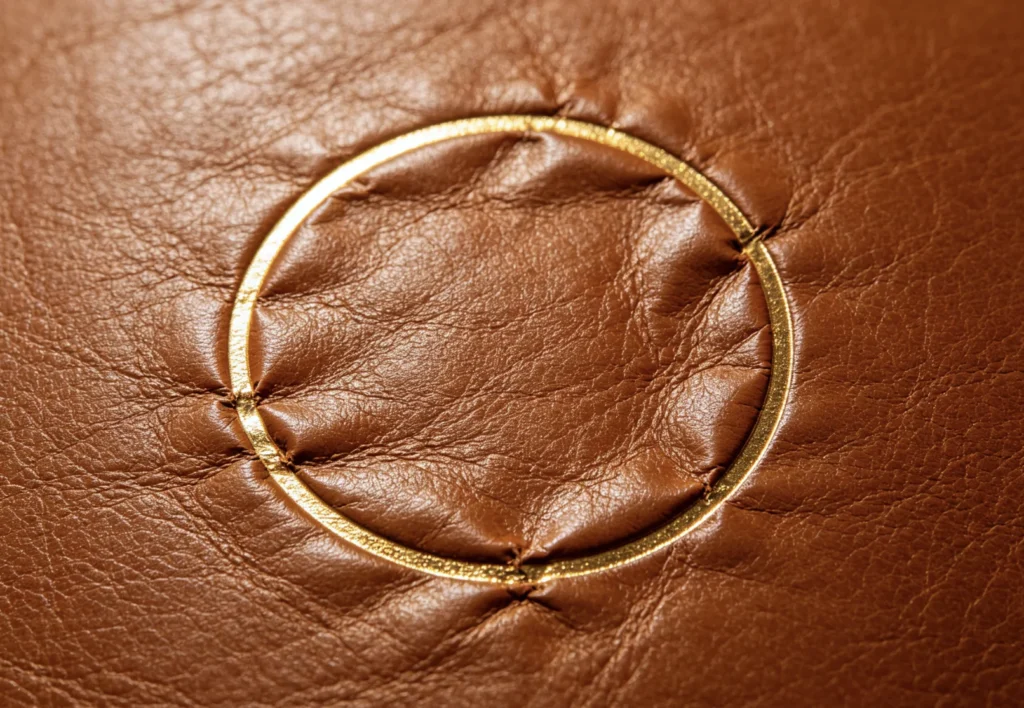
Soft leather compresses easily. If the leather piece sits on a soft or uneven surface, the die may push the material downward instead of creating a controlled surface impression.
This is especially common with:
Use a firm, flat support under the stamping area whenever possible. For finished products, avoid stamping over seams, folds, zippers, padded areas or raised edges.
If the product cannot lie flat, the risk of deep marks and uneven foil transfer increases.
When the die is not level, one side contacts first. The operator may increase pressure to make the weak side transfer, but then the strong side becomes too deep.
Signs of uneven die contact:
Before changing temperature, check die flatness and machine alignment. A small leveling issue can create a big difference in leather results.
Foil stamping, blind debossing and heat branding are different effects.
If the customer wants a deep permanent mark, blind debossing or heat branding may be more suitable than foil stamping. If the customer wants clean gold, silver or colored foil, a shallow controlled impression is usually safer.
Forcing a foil stamp to become very deep often creates messy foil and leather damage. A Reddit leathercraft discussion on gold stamp embossing made the same practical point: clean foil and deep impression often require different priorities.
For choosing the process, see Embossing vs Foil Stamping vs Heat Branding.
| Symptom | Likely Cause | Fix |
|---|---|---|
| Logo is too deep but foil is clean | 압력이 너무 높음 | reduce pressure or use a firmer backing |
| Leather is shiny around the logo | pressure too high or heat softening coating | reduce pressure, temperature or dwell time |
| PU leather wrinkles | heat and pressure are too aggressive | lower temperature and shorten dwell time |
| Small letters spread | temperature, pressure or time too high | reduce heat/time and review letter spacing |
| One side is deep, one side is weak | die not level or support uneven | level the die and improve backing support |
| Foil transfers outside the logo | pressure/heat too high or foil releases too easily | lower temperature and test another foil |
| Center of large logo is weak | die area too large or pressure uneven | use a more stable press or redesign the die |
Change only one variable at a time. If you reduce pressure, temperature and dwell time together, you may not know which change solved the problem.
Use this process before stamping final leather goods:
Flat leather scrap is useful, but it is not always enough. If the final product is a finished wallet, bag or notebook cover, test a similar product structure because padding, backing and seams change the pressure result.
| Project Type | Better Tool Path | Why |
|---|---|---|
| Small leather names and initials | EC-27 수동 열압 인쇄기 | useful for compact leather personalization and controlled small-area stamping |
| PU leather thick letter stamping | WT-90XTS 수동 핫 스탬핑 기계 | suitable for thick letter type and small-batch leather work |
| Simple flat leather samples | EC-17 수동 열압 인쇄기 | practical for small flat work and paper/card testing |
| Larger leather panels or book covers | 618-M 공압식 핫 스탬핑 기계 | larger work area and more repeatable pressing for bigger jobs |
| Deep relief or heavy pressure work | YTJ-5T 유압식 핫 스탬핑 프레스 | stronger controlled pressure for suitable embossing and 3D work |
| Burned leather or wood marks | 맞춤 황동 브랜드 아이언 | better when the desired effect is heat branding, not foil transfer |
For machine selection, read 가죽 제품에 가장 적합한 핫 스탬핑 기계 선택 방법 및 EC-17 대 EC-27 핫 호일 스탬핑 기계.
PU leather can produce clean foil results, but the coating is sensitive to heat and pressure. If it gets too hot, it can soften, wrinkle, harden or show permanent pressure marks.
Start conservatively and avoid chasing a stronger metallic shine by adding too much heat. If the foil already transfers, reduce pressure or dwell time when press marks appear.
Genuine leather varies more than PU leather. Full-grain, corrected grain, split leather, oily leather and soft leather can all respond differently.
Some genuine leather accepts a shallow foil stamp well. Other leather may darken, polish, flatten or resist foil. Oily leather can be difficult because surface oils may interfere with adhesion.
Finished wallets, bags, journals and covers are harder than flat leather pieces. They may have seams, padding, board, glue layers or curved areas under the stamping location.
Before production, check whether the stamping area can lie flat and receive even backing support.
Sometimes the customer wants a deep blind deboss instead of foil. In that case, the process should be planned differently.
For blind debossing:
For foil stamping:
If the customer wants both depth and metallic color, consider whether a 3D relief die or two-step process is more suitable. Read 포일 스탬핑 전에 사전 엠보싱이 필요할까요?.
When a customer says hot stamping leaves deep marks on leather, ask for:
These details help separate material problems from machine setup, die contact and process settings.
Hot stamping leaves a deep mark when pressure, temperature or dwell time is too high for the leather, or when the die area is too large and the material is too soft. Reduce pressure first if the foil is already transferring, then adjust heat and dwell time.
Not necessarily. For clean metallic foil, a shallow and even impression is often better than a deep one. Deep debossing is a different effect and should be planned intentionally.
Reduce pressure, lower temperature if the leather coating is softening, shorten dwell time, and use firm flat backing under the material. Also avoid stamping over seams, padding or uneven product areas.
PU leather can deform when the coating softens under heat and pressure. High temperature, long dwell time, strong pressure or a large solid die can create wrinkles, dents, fuzzy edges or permanent marks.
Usually not completely. Some minor shine may reduce with time or gentle leather care, but deep deformation, melted coating or scorch marks are often permanent. It is better to prevent the problem through testing.
It can be caused by either, but the full system matters: die size, relief height, machine pressure, backing support, leather softness, temperature and dwell time. Test the same die on scrap material before judging the machine.
Based on Zhengfei tests, 100-110°C with short dwell time is a practical starting range for several PU leather foil stamping jobs, depending on machine and die type. Always test your actual PU leather, foil and logo size before production.
Need to reduce deep marks, shiny pressure areas or leather deformation during hot foil stamping?
Send ZHENGFEI your material photo, failed stamping photo, logo size, machine model, foil type, temperature and dwell time. Our team can help review whether the issue comes from pressure, heat, die design, leather type or machine selection.

 English English
 Japanese
 Spanish
 French
 Korean
 German
 Russian