We use cookies to ensure that we give you the best experience on our website.
Contact Founder
Still have doubts?
Connect directly with our Founder. Whether it’s about pricing or technical details, get a straight answer and an exclusive “Founder’s Bonus” for your first order.
900+ Satisfied Clients
🏆 Over 1000+ Custom Projects Successfully Delivered.
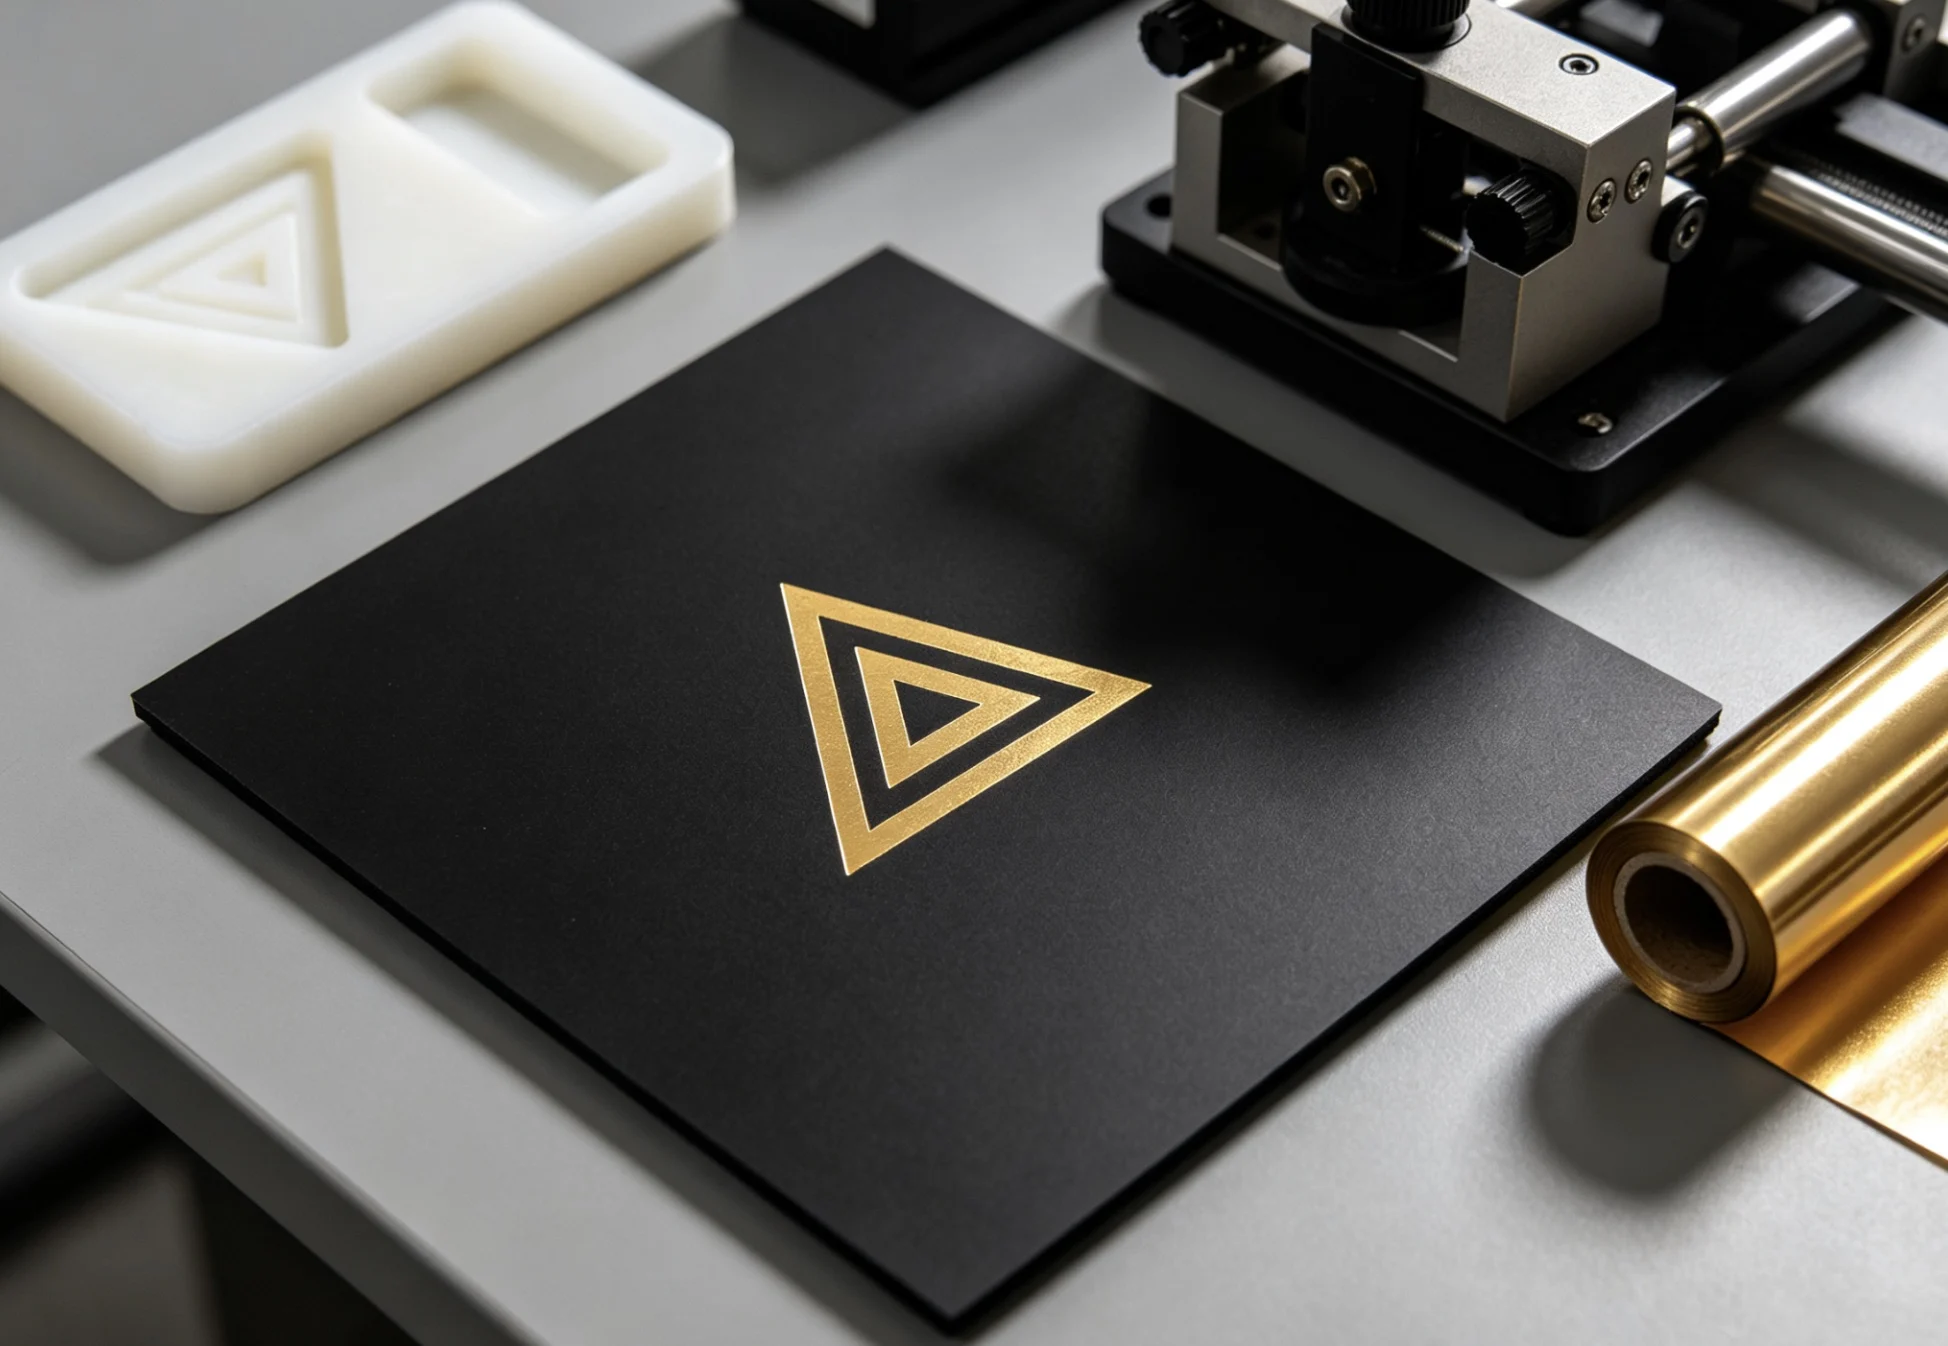
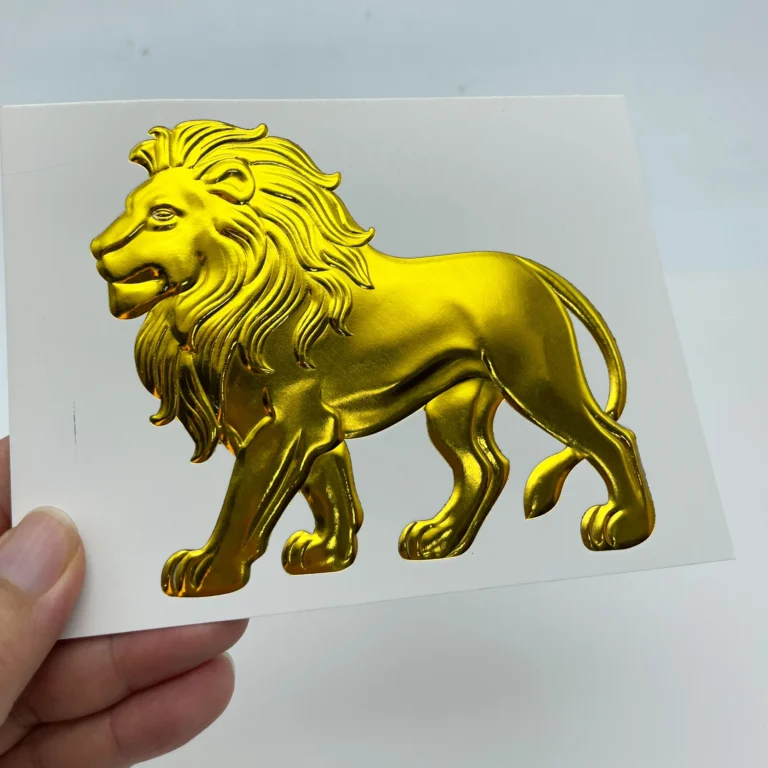
Factory‑direct hot stamping delivers crisp metallic gold logos on ABS plastic with 0.01‑mm precision engraving.
Best ABS Plastic Foil Stamping Temperature: TJ8020PS Test at 170-200°C
We tested hot foil stamping on ABS plastic with a TJ8020PS hot stamping machine and silicone mold at 170°C, 180°C, 190°C, and 200°C. The best result came at 190°C for 1 second, with stable foil transfer, clear edges, good metallic gloss, and lower risk of ABS surface softening or deformation.
What is the best ABS plastic foil stamping temperature? In the documented ZHENGFEI test, the best reference result came from 190°C for 1 second using a TJ8020PS hot stamping machine, a silicone mold、および ABS plastic.
The test compared 170°C, 180°C, 190°C, and 200°C. At 170°C, the foil release was not complete enough, so fine lines and complex details could show missing foil or weak transfer. At 180°C, transfer improved, but some fine or complex areas could still be slightly incomplete. At 190°C, the foil transferred more fully with better gloss, cleaner edges, and stronger overall stability. At 200°C, transfer could become fuller, but the ABS surface faced higher risk of softening, deformation, pressure marks, and edge spread.
This article is for plastic product manufacturers, electronic shell factories, automotive interior suppliers, appliance accessory makers, daily-use product factories, and OEM buyers who need metallic logos, lettering, or decorative graphics on ABS parts. The 190°C setting is a test reference, not a fixed rule for every ABS grade, foil, mold, or product shape.
Quick Answer: What Temperature Should You Use for ABS Plastic Foil Stamping?
For the tested combination of TJ8020PS, silicone mold, and ABS plastic, start with:
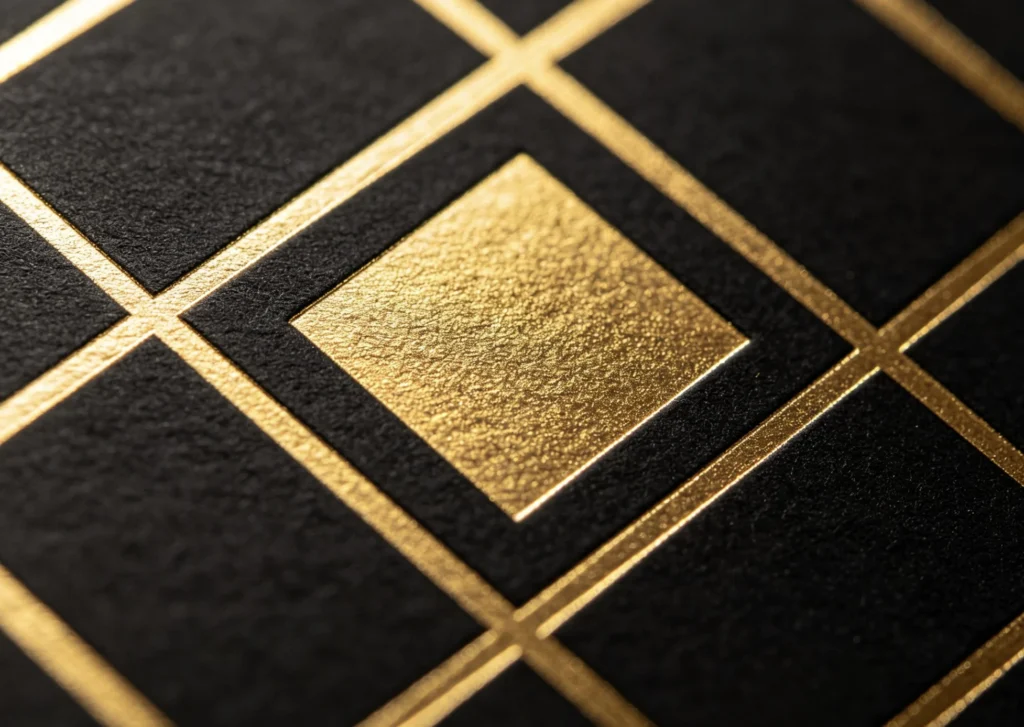
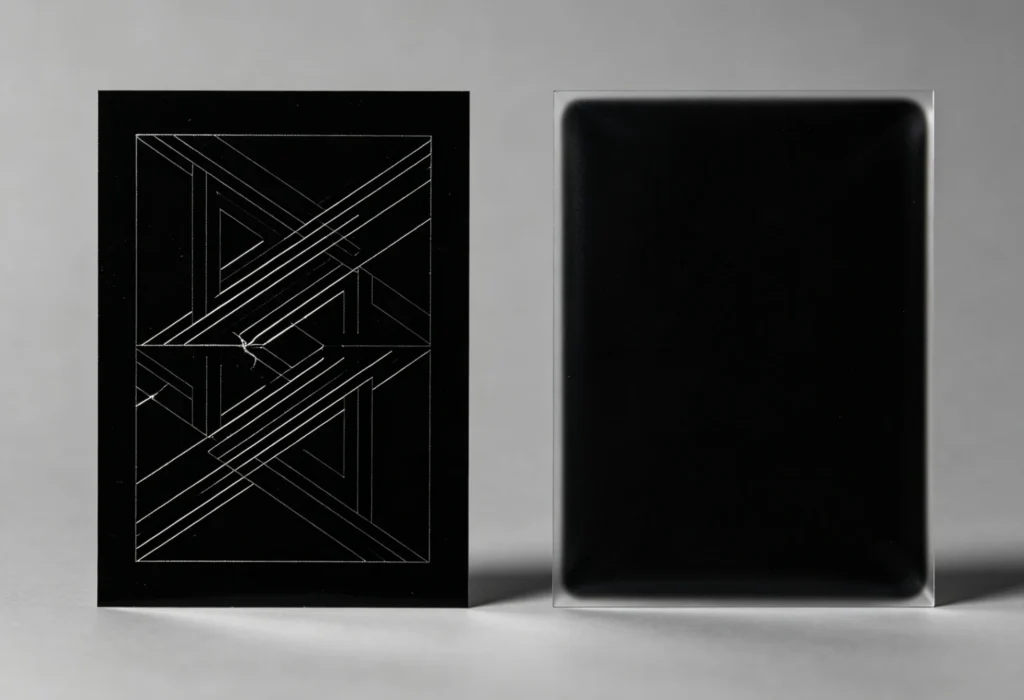
High‑precision 0.01 mm engraving reproduces ultra‑fine lines without edge blur on ABS plastic components.
Use 190°C for 1 second as the first sampling point when your ABS part, foil, and silicone mold are similar. If transfer is incomplete, check mold contact, pressure, foil type, and surface cleanliness before raising the temperature. If the ABS surface softens, deforms, or shows marks, reduce heat, shorten dwell time, or lower pressure.
For another plastic material, compare our acrylic foil stamping temperature test. Acrylic and ABS both need heat control, but they do not behave the same under pressure and temperature.
Why ABS Plastic Needs Controlled Heat During Foil Stamping
ABS plastic, short for acrylonitrile butadiene styrene, is widely used because it has good mechanical strength and practical surface processing performance. It is common in electronic housings, automotive interior parts, appliance accessories, daily-use plastic products, and industrial components. A general material reference is available from this overview of acrylonitrile butadiene styrene, and the material classification system is covered by ASTM D4673-23.
ABS is useful for decorative finishing because logos, brand text, symbols, and metallic lines can improve the product’s perceived value. A clean foil logo on an ABS shell can make a functional plastic part look more premium, especially for electronics, cosmetic packaging components, control panels, and branded accessories.
However, ABS is a thermoplastic material. That means the surface can respond visibly when heat and pressure are too high. During hot foil stamping, the process must provide enough heat for the foil layer to release and bond, while avoiding surface softening, abnormal pressure marks, or shape change.
The result depends on several variables working together:
温度
停留時間
Pressure level
Pressure uniformity
Silicone mold hardness
ABS grade and surface condition
Product thickness and support
Foil model and release temperature
Artwork size and line detail
This is why one number cannot be copied blindly across every ABS product. The documented 190°C / 1-second condition is a strong starting reference, but final production should always be confirmed with the real product.
Why a Silicone Mold Helps on ABS Plastic Parts
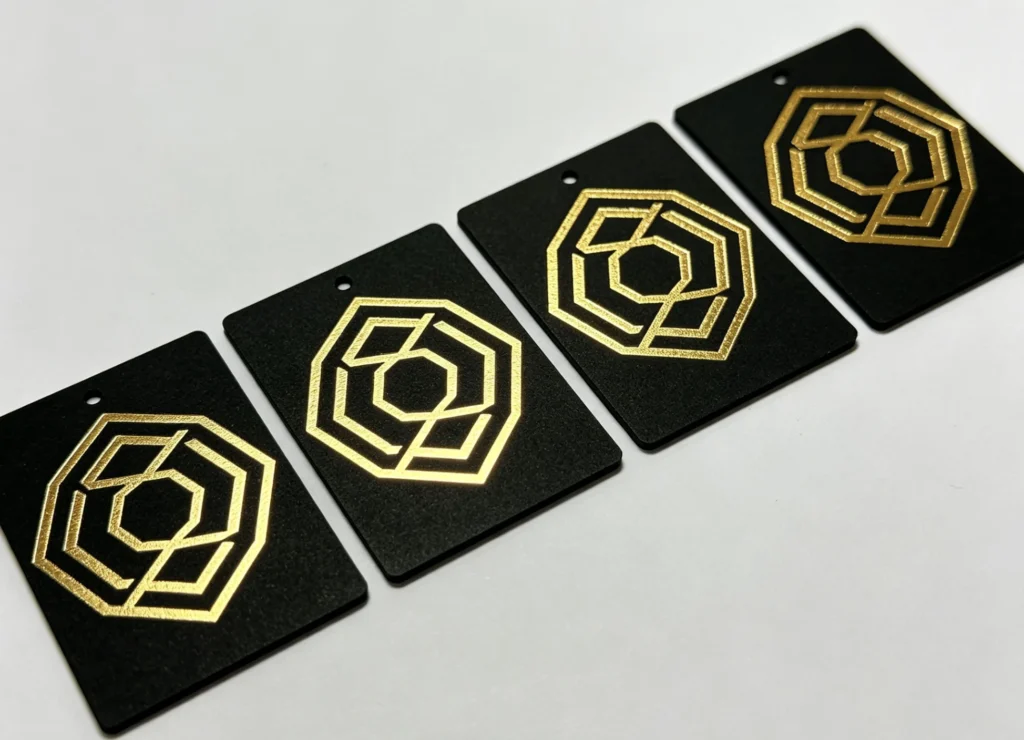
Consistent repeatable foil stamping output for ABS plastic tags, free design service available for custom patterns.
The source test used a silicone mold instead of a rigid metal die. Silicone has elasticity and flexibility; a general material reference is available here: silicone.
This matters because ABS products are often not perfectly flat. Many parts have slight curves, raised areas, recessed edges, ribs, or local height differences. A silicone mold can adapt better to these surfaces during pressure, helping the foil stay in more complete contact with the plastic.
Compared with a hard metal die, a silicone mold can reduce local pressure concentration and improve the consistency of foil transfer across slightly uneven areas. This is especially useful for small logos, curved plastic surfaces, and decorative patterns on molded parts.
That does not mean silicone solves every problem. The mold still needs to be clean, correctly mounted, and matched to the part shape. If the silicone surface has foil dust, residue, wear, or uneven contact, the result can still show missing foil, blurry details, or inconsistent gloss.
Temperature Comparison: 170°C, 180°C, 190°C, and 200°C
The following summary follows the original ABS plastic test report.
Compare silicone tool against finished ABS stamped output; factory‑direct pricing saves 30‑50 % vs trading companies.
温度
Observed transfer behavior
Surface and production judgment
170°C
Foil release was not sufficient. Fine text, thin lines, and complex patterns could show missing foil or incomplete transfer.
Too low for a stable reference result
180°C
Transfer improved. Most graphics became visible, with better gloss and clearer edges, but fine or complex areas could still be incomplete.
Improved, but not the best result
190°C
Foil transferred more fully and evenly. Gloss, edge clarity, and detail restoration were more balanced.
Recommended reference in this test
200°C
Transfer could become fuller, especially on larger areas, but ABS heat risk increased.
Use cautiously; not recommended as a default
170°C: Foil Transfer Was Not Complete Enough
At 170°C, the metallic layer did not release and transfer sufficiently to the ABS surface. Fine text, thin strokes, and complicated artwork were more likely to show missing foil, broken lines, or local incomplete transfer.
The metallic gloss was also weaker at this setting. For ABS, the lower temperature helps reduce heat impact, but it does not create a good production result if the foil cannot attach fully.
If a factory sees incomplete transfer at a low temperature, it should not only raise heat. First check whether the foil is suitable for ABS, whether the silicone mold is touching evenly, whether the pressure is too light, and whether the plastic surface is clean. For a broader diagnostic path, read why foil does not transfer.
180°C: Better Transfer but Still Not Fully Stable
At 180°C, foil transfer became more stable compared with 170°C. Most of the artwork could appear, the metallic gloss improved, and the edges became clearer.
However, the report still notes possible transfer insufficiency in fine text and complex texture areas. This means 180°C may be usable for simple designs, but it may not be stable enough for detailed logos or demanding product surfaces.
For sample development, 180°C can be useful as a lower-risk comparison point. It helps show whether the foil and ABS surface are generally compatible before moving toward the 190°C reference condition.
190°C: The Recommended Reference Condition
The report identifies 190°C as the recommended reference temperature. At 190°C for 1 second, the foil transferred more sufficiently to the ABS surface. The metallic gloss looked better, the graphic edges were clearer, and the design details were restored more accurately.
The silicone mold helped by conforming to the ABS surface and improving pressure contact. This made the transfer more uniform and reduced the risk of local incomplete areas.
The 1-second dwell time is important. ABS does not benefit from long heat exposure. A short cycle allows the foil layer to transfer while reducing the risk that the plastic surface will soften, deform, or show abnormal marks.
For this tested combination, 190°C / 1 second is the best sampling reference. It should still be verified on the actual ABS grade, product surface, foil model, silicone mold, and production fixture.
200°C: Fuller Transfer but Higher Plastic Surface Risk
At 200°C, foil transfer may become more complete, and larger areas can look fuller. But the report warns that higher temperature can increase the risk of ABS surface softening, deformation, or pressure marks.
Fine details may also suffer. When heat is too high, edges can spread and small features can become less sharp. This is a common production trap: a higher temperature may improve coverage, but it can also reduce precision.
For ABS products, do not raise temperature just to make the foil look more saturated. Check pressure, dwell time, foil type, and mold contact first. The goal is not maximum heat; the goal is the most stable balance between foil transfer and surface protection.
How to Adjust ABS Plastic Foil Stamping in Real Production
Use 190°C / 1 second as a starting point for similar ABS plastic parts. Then make small adjustments based on product structure and test results.
Step 1: Identify the ABS Product Structure
ABS products can be flat, curved, textured, ribbed, coated, painted, or assembled with other parts. The product shape affects pressure distribution and heat response.
Before testing, confirm:
ABS grade or supplier batch
Surface finish: glossy, matte, textured, painted, or coated
Product thickness
Whether the stamping area is flat or curved
Whether the part has ribs, seams, edges, or height differences near the stamp
Whether the plastic part can be supported from underneath
Step 2: Clean the Surface and Mold
Dust, oil, release agent, fingerprints, and foil residue can interrupt transfer. Clean both the ABS surface and silicone mold before testing.
The silicone mold should also be inspected for wear. If the mold surface is damaged or contaminated, the stamping problem may look like a temperature issue even when the machine setting is correct.
Step 3: Start with the 190°C / 1-Second Reference
For a similar ABS part and silicone mold, begin with 190°C and 1 second. Test both fine detail and larger areas.
Do not approve production from a single simple logo sample. A complete test should include:
Fine text
Thin lines
Small internal gaps
Curved areas if the product is curved
Any larger solid logo area
Real product support fixture
Step 4: Adjust One Variable at a Time
If transfer is incomplete, first check pressure and contact. If those are stable, increase temperature slightly or test another foil model.
If edges spread, details blur, or the surface shows marks, reduce temperature, pressure, or dwell time. Avoid changing everything at once, because then you will not know which adjustment actually fixed the problem.
ABS plastic parts may vary between batches. Foil rolls, mold wear, operator pressure, and machine temperature stability can also affect the final result.
Before batch production, record:
Machine model
温度
停留時間
Pressure setting
Foil model
ABS material batch
Mold hardness and condition
Product fixture method
Approved visual sample
This record helps reduce batch-to-batch differences. It also makes future reorders easier to control.
Common ABS Plastic Foil Stamping Defects and Fixes
Defect
Likely cause
First checks
箔の欠落
Temperature too low, weak pressure, poor mold contact, unsuitable foil
Check surface, mold contact, pressure, and foil before raising heat
Broken thin lines
Fine artwork, incomplete foil release, dirty mold
Clean the mold and test near the 180-190°C range
Weak metallic gloss
Foil not fully transferred or pressure is uneven
Improve contact and confirm foil compatibility
Blurry edges
Temperature too high or pressure too heavy
Reduce heat or pressure and inspect artwork size
Surface softening
Heat exposure is too high
Lower temperature or shorten dwell time
Pressure marks
Excessive pressure or uneven support
Improve product support and reduce pressure
Deformation
Too much heat, too long dwell time, weak fixture support
Shorten dwell time and support the part from below
Foil peeling
Weak adhesion or foil/surface mismatch
Test a better-matched foil and allow stable cooling
ABS vs Acrylic: Why the Same 190°C Test Point Does Not Mean the Same Process
The ABS test and the acrylic foil stamping temperature test both used a 190°C / 1-second reference with TJ8020PS and a silicone mold. That similarity is useful, but it does not mean ABS and acrylic behave the same.
Acrylic is valued for transparency and gloss. Surface marks and gloss changes are very visible. ABS is more common in molded functional parts, and the key risks often include surface softening, deformation, pressure marks, and loss of edge definition.
Both materials require controlled heat, short dwell time, suitable foil, and stable pressure. But the final setting should still be confirmed separately for each material and product shape.
The documented source test used a TJ8020PS hot stamping machine. At the time of this article draft, the ZHENGFEI sitemap does not show a live TJ8020PS product page, so the schema related product should use the ZHENGFEI hot stamping machines category until a dedicated TJ8020PS page is available.
For different production needs, these machine pages may also be useful:
For a project-specific ABS test, fixture review, foil selection, or machine recommendation, contact ZHENGFEI.
Frequently Asked Questions
What is the best ABS plastic foil stamping temperature?
In the documented TJ8020PS test, 190°C was the best reference temperature for ABS plastic with a silicone mold. The recommended condition was 190°C for 1 second. Always test the actual ABS grade, product surface, foil, mold, and fixture before batch production.
Can you hot foil stamp ABS plastic?
Yes. ABS plastic can be hot foil stamped when temperature, pressure, dwell time, foil type, and mold contact are matched correctly. Silicone molds are useful for ABS products with slight curves, height differences, or surfaces that need flexible pressure contact.
Why does foil not transfer completely on ABS?
Common causes include low temperature, weak pressure, uneven silicone-mold contact, unsuitable foil, dirty ABS surface, or artwork details that are too fine. Check surface cleanliness and mold contact before increasing temperature.
Why does ABS deform during hot stamping?
ABS can deform when heat exposure is too high, dwell time is too long, pressure is too heavy, or the product is not supported properly from underneath. Reducing heat, shortening dwell time, and improving fixture support can lower the risk.
Is 200°C too high for ABS foil stamping?
In this test, 200°C could make foil transfer fuller, but it also increased the risk of ABS softening, deformation, pressure marks, edge spread, and blurred details. It should not be used as the default setting without product-specific testing.
Is silicone mold better than brass die for ABS?
A silicone mold is often better for ABS parts with curved, uneven, or slightly irregular surfaces because it can provide flexible contact. A brass die may be better for flat parts that need very sharp engraved edges and long-term repeated production.
結論
For the tested combination of TJ8020PS hot stamping machine + silicone mold + ABS plastic, the best ABS plastic foil stamping temperature was 190°C for 1 second.
At 170°C, foil transfer was incomplete. At 180°C, transfer improved but was not fully stable in fine or complex areas. At 190°C, the result was more balanced, with good gloss, clearer edges, and stronger detail restoration. At 200°C, transfer could become fuller, but the risk of ABS softening, deformation, pressure marks, edge spread, and blurred details increased.
Use 190°C / 1 second as a practical starting reference, then confirm the result with the actual ABS material, foil, silicone mold, artwork, pressure, dwell time, and product support. If you need help choosing a machine, designing a mold, or testing ABS product decoration, contact ZHENGFEI.
Author and Test Note
This article is based on a ZHENGFEI process test prepared by John Zhao, founder of ZHENGFEI. The company has more than 21 years of experience covering graphic design, book and packaging printing, hot stamping processes, equipment selection, custom mold production, and production support. The test value is a practical reference; it should not replace a sample test on the buyer’s actual ABS material and production structure.
あなたの愛を分かち合いましょう
ZHENGFEI Technical Team
ZHENGFEI Technical Team shares practical hot stamping knowledge from real production tests, including brass die design, foil stamping parameters, machine setup, leather, paper, acrylic, plastic, wood and packaging applications.

 English
 Japanese
 Spanish
 French
 Korean
 German
 Russian